


How does digital surfacing revolutionize lenses manufacturing?
- 1) How can I verify an eyewear factory's digital surfacing capacity for high-volume customized orders (units/day, machine types, automation)?
- 2) What specific QC metrics and inspection reports should an eyewear factory provide for digitally surfaced lenses to guarantee prescription accuracy and AR coating adhesion?
- 3) Are digital surfacing processes compatible with high-index, polarized, and photochromic materials without increasing rejection rates?
- 4) What is the realistic lead time and bottleneck breakdown when ordering digitally surfaced custom progressive lenses from an eyewear factory?
- 5) How does retrofitting an existing eyewear factory with freeform digital surfacing affect ROI, footprint, and workforce training?
- 6) What traceability and data-security practices should I require from an eyewear factory to protect patient data and ensure batch-level traceability for recalls?
As eyewear procurement managers, independent optical labs, or brand product leads evaluate suppliers, digital surfacing (freeform CNC generation) is the single biggest production shift in the last decade. Below are six highly specific, pain-point-oriented questions buyers and beginners frequently ask but rarely find complete answers to online. Each reply gives actionable checks, measurable criteria, and vendor/integration considerations you can use when auditing an eyewear factory, optical lab, or lens lab.
1) How can I verify an eyewear factory's digital surfacing capacity for high-volume customized orders (units/day, machine types, automation)?
Why this matters: Procurement often receives vague statements like “we have freeform surfacing.” For commercial planning you need machine throughput, redundancy, and the factory’s real blocker-to-box lead time—not marketing speak.
Actionable verification checklist:
- Request an equipment inventory: list brand/model/age for surfacers (e.g., Satisloh, OptoTech, Schneider) and supporting machines (blockers, tracers, polishers, coaters). Ask for spindle RPM, tool life policies, and whether multiple recipes/tool sets exist for different materials (CR-39, polycarbonate, Trivex, 1.67/1.74).
- Ask for demonstrated throughput metrics: average surfacing time per lens (minutes), blocker/tracer cycle times, batch coating cycle times, and OEE (overall equipment effectiveness) or uptime percentages for the last 6–12 months. If the factory cannot provide, treat this as a red flag.
- Get shift and staffing patterns: single-shift vs 24/7, operator-to-machine ratios, and on-site maintenance resources. High-volume customized runs require at least two shifts or automated pallet loaders to meet daily quotas without overtime spikes.
- Verify bottleneck points with a value-stream map from order receipt to shipment. Common bottlenecks: AR coating capacity, curing ovens (batch cycles), and manual edging/inspection hands-on steps. A factory should produce a time-in-process breakdown (hours per stage) for typical orders.
- Request a pilot run or sample schedule: a verified pilot (10–50 prescriptions) gives empirical throughput and defect rates. Ensure the sample includes high-index and wrap prescriptions if you plan to ship those volumes.
Red flags: unwillingness to share cycle-time data, no separate tooling/recipes for high-index/photochromic blanks, and a single coating line serving all orders (creates single-point delays).
2) What specific QC metrics and inspection reports should an eyewear factory provide for digitally surfaced lenses to guarantee prescription accuracy and AR coating adhesion?
Why this matters: Prescriptions and coatings directly affect patient satisfaction and liability. A factory must provide objective, machine-readable QC artifacts—not only “passed inspection” stickers.
Essential QC deliverables to request:
- Power and prism maps (power profile / power uniformity). These are numerical maps (CSV or PDF) showing measured sphere/cylinder across the lens surface. Look for the factory’s target tolerances and actual results per job.
- Surface form error / interferometric profile (if available) or surface roughness Ra values. Modern freeform surfacing aims for sub-micron surface figure accuracy and nm-level roughness for good AR adhesion.
- Center thickness and edge thickness reports tied to the job ID; these should match the blocking and final edge specs. Thickness deviations can indicate grinding or material swell issues.
- Centration and tilt / decentration metrics: horizontal and vertical centration (in mm) and any tilt/pantoscopic compensation applied. For progressive lenses, provide inset and corridor position confirmation.
- Coating adhesion and durability test results: cross-hatch adhesion, abrasion cycles (Taber or specified cycles), and sample UV/salt-fog tests for sunglasses/coatings when relevant. Ask for batch numbers of coating materials and curing cycle logs.
- Remake/failure rates per job and root-cause records for the last 6–12 months (e.g., % remakes due to surfacing error, coating defects, blocking). A modern digital lens lab should track and attribute defects to specific machines/recipes.
Acceptable target ranges (industry practice): many labs aim for power accuracy within ±0.12–0.25 D for finished single-vision lenses, axis within ±2° for cylinders, and centration to within 0.2–0.5 mm for progressive fitting zones. However, tolerances vary by standard (see ISO 8980 and ANSI Z80.1) and by lens type—confirm the factory’s published spec and ask for matching measurement artifacts.
3) Are digital surfacing processes compatible with high-index, polarized, and photochromic materials without increasing rejection rates?
Why this matters: Buyers expect material flexibility. Digital surfacing is compatible with most optical blanks, but material-specific process control is crucial to keep rejects low.
Technical compatibility notes:
- Material-specific tooling and spindle settings: high-index resins (1.67, 1.74) are more brittle and denser—tool speed, feed, and coolant parameters must be validated. Many factories maintain separate tool sets and surfacing recipes per material.
- Stress and birefringence control: polycarbonate and Trivex show more residual stress potential. Proper blocking, pre-annealing (for some materials), and surfacing feed rates reduce surface/sub-surface stress that causes visual artifacts.
- Polarized and laminated lenses: polarized films are often laminated to a carrier blank—surfacing must be validated to avoid delamination. Some surfacers limit material thickness or require specific blocker types to protect the film during machining.
- Photochromic dyes/stocks: photochromic blanks from major suppliers (Transitions, Hoya, Essilor lenses) are routinely surfaced on freeform machines but require validated coating adhesion and post-surfacing cure cycles. Ask for adhesion data specific to the vendor’s photochromic batch you plan to use.
What to ask the factory for:
- Material-specific process sheets and sample reports for each material type you intend to order (including rejection rates by material for the last 12 months).
- Evidence of separate tool inventories or changeover SOPs that prevent cross-contamination and preserve surface quality for laminated/polarized work.
- Sample lenses surfaced from the exact material batches you’ll supply or plan to buy through them.
4) What is the realistic lead time and bottleneck breakdown when ordering digitally surfaced custom progressive lenses from an eyewear factory?
Why this matters: Shipping timelines determine inventory strategy and customer lead promises. Digital surfacing speeds some steps but does not remove coating and inspection bottlenecks.
Typical process stages and time ranges (factory-dependent):
- Order entry & Rx verification: same day to 24 hours (automated systems can shorten this).
- Blocking and centering: 15–60 minutes per lens or batch parallelized with automatic blockers.
- Surfacing (freeform generation): 5–30 minutes per lens depending on complexity and machine settings.
- Fine-polish/smoothing or deterministic polish: 15–60 minutes per lens if needed.
- AR coating: batching and oven cycles typically add 12–48 hours (coating load and cure cycles are common bottlenecks).
- Edging and frame-fit: 30–90 minutes depending on frame complexity and edge finishing requirements.
- Final inspection, packing, and shipping: same day to 24 hours.
Realistic total lead times:
- Single-vision with standard coatings (in-stock blanks): 24–72 hours in high-capacity labs.
- Custom progressive with AR/photochromic/high-index: commonly 3–7 business days, driven primarily by coating batch cycles and inspection throughput.
- Large bespoke orders: plan for 1–3 weeks, depending on blank procurement and coater capacity.
How to reduce lead time:
- Negotiate dedicated coating slots or priority runs (often available as a High Quality service).
- Pre-stock high-use blanks (high-index, special tints) at the factory or in a bonded stock location to avoid procurement delays.
- Automate job submission and blocking with industry-standard job tickets to reduce hand-offs.
5) How does retrofitting an existing eyewear factory with freeform digital surfacing affect ROI, footprint, and workforce training?
Why this matters: Many mid-size factories weigh buying surfacers and controllers versus continuing to outsource. The correct retrofit plan balances capex, OPEX, and production scalability.
Capital and operational considerations:
- Capital equipment: a modern freeform surfacer plus tracer/blocker and a basic coater/polisher can be a significant investment. Depending on automation level and brand, buyers typically plan for a wide capex range—evaluate vendor quotes for total installed cost including automation arms, palletizers, and software licenses.
- Factory footprint: surfacing machines are compact, but supporting equipment (coaters, curing ovens, waste handling) and space for staging and inspection increase footprint requirements—plan 1.2–1.6x existing bench space per new production line when adding coating capability.
- Workforce and training: operators need CNC recipe management skills, metrology interpretation (power maps and surface profiles), and routine maintenance competence. Vendors (Satisloh, OptoTech, Schneider, etc.) typically supply multi-day on-site training plus follow-up service contracts. Expect a 4–12 week learning curve for consistent first-pass yield.
- ROI considerations: savings derive from reduced outsourcing costs, lower remake rates, faster cycles, and higher-margin customized products. Many labs see payback in 12–36 months depending on utilization, product mix, and labor savings—but run a conservative scenario analysis with actual volumes before committing.
Best practice: start with a pilot freeform cell (one surfacer, one blocker/tracer, minimal coating outsourcing) to quantify yield and cycle times, then scale. Maintain strong OEM service agreements and spare-part inventories to minimize downtime.
6) What traceability and data-security practices should I require from an eyewear factory to protect patient data and ensure batch-level traceability for recalls?
Why this matters: Prescription data is personal; batch-level traceability is critical for safety recalls and warranty claims. Ask for concrete, auditable controls—not just promises.
Essential traceability and security requirements:
- Digital job tickets with unique job IDs: include lens prescription, centration parameters, material batch numbers, coating batch IDs, machine ID, operator ID, and timestamp for each process step.
- Serialized lens identifiers and QR-coded packaging: allow scanning back to the full job history (surfacer settings, inspection maps, coating batch). This simplifies recalls and warranty investigations.
- Access controls and encrypted Rx transfer: require TLS-encrypted uploads, role-based access controls, and retention policies compliant with GDPR for EU customers. If handling protected health information in the US, confirm HIPAA alignment where applicable.
- Audit logs and MES/ERP integration: factory should provide exportable audit logs and a documented API or EDI connector to integrate order and trace data into your systems. Request examples or sandbox access during vendor evaluation.
- Supplier and material traceability: coating chemicals, blank suppliers, and lot numbers should be recorded. Prefer vendors that retain these records for at least 2–5 years and have recall SOPs.
Verification steps during factory audit: review job-ticket samples, scan a QR code to trace a finished lens back through surfacing and coating, and request read-only access to recent audit logs. If the factory resists data transparency, require contractual SLAs that mandate traceability delivery.
Standards and certification to look for: ISO 9001 quality management, adherence to ISO 8980 series for optical properties, and compliance with regional standards such as ANSI Z80.1 (US) or CE marking for medical claims in the EU. For data protection, look for GDPR compliance statements and documented security controls (encryption, RBAC, logging).
Contact us for a tailored audit checklist and a pilot-run quote that verifies capacity, QC artifacts, and lead-time commitments.
To request samples, a capacity audit, or a quote, contact Karuson Optical Solutions at www.karusonco.com or email nicole@karusonco.com.
Conclusion — Advantages of digital surfacing and modern eyewear factory practices: Digital surfacing (freeform generation) modernizes lens production by enabling fully customized optics—precise centration, personalized progressive geometry, correction for frame wrap and pantoscopic tilt, and reproducible surface form across lots. When integrated with validated coatings, automated blocking/tracing, and ERP/MES traceability, digital surfacing reduces manual finishing, shortens lead times for many SKUs, and improves first-pass fit. For buyers, the combination results in fewer remakes, better patient satisfaction, and the ability to scale customization without linear increases in labor. For a factory audit, prioritize measurable QC artifacts, material-specific process validation, reliable coating throughput, and robust traceability.
Contact us at www.karusonco.com or nicole@karusonco.com to arrange a pilot run or request a detailed quote.
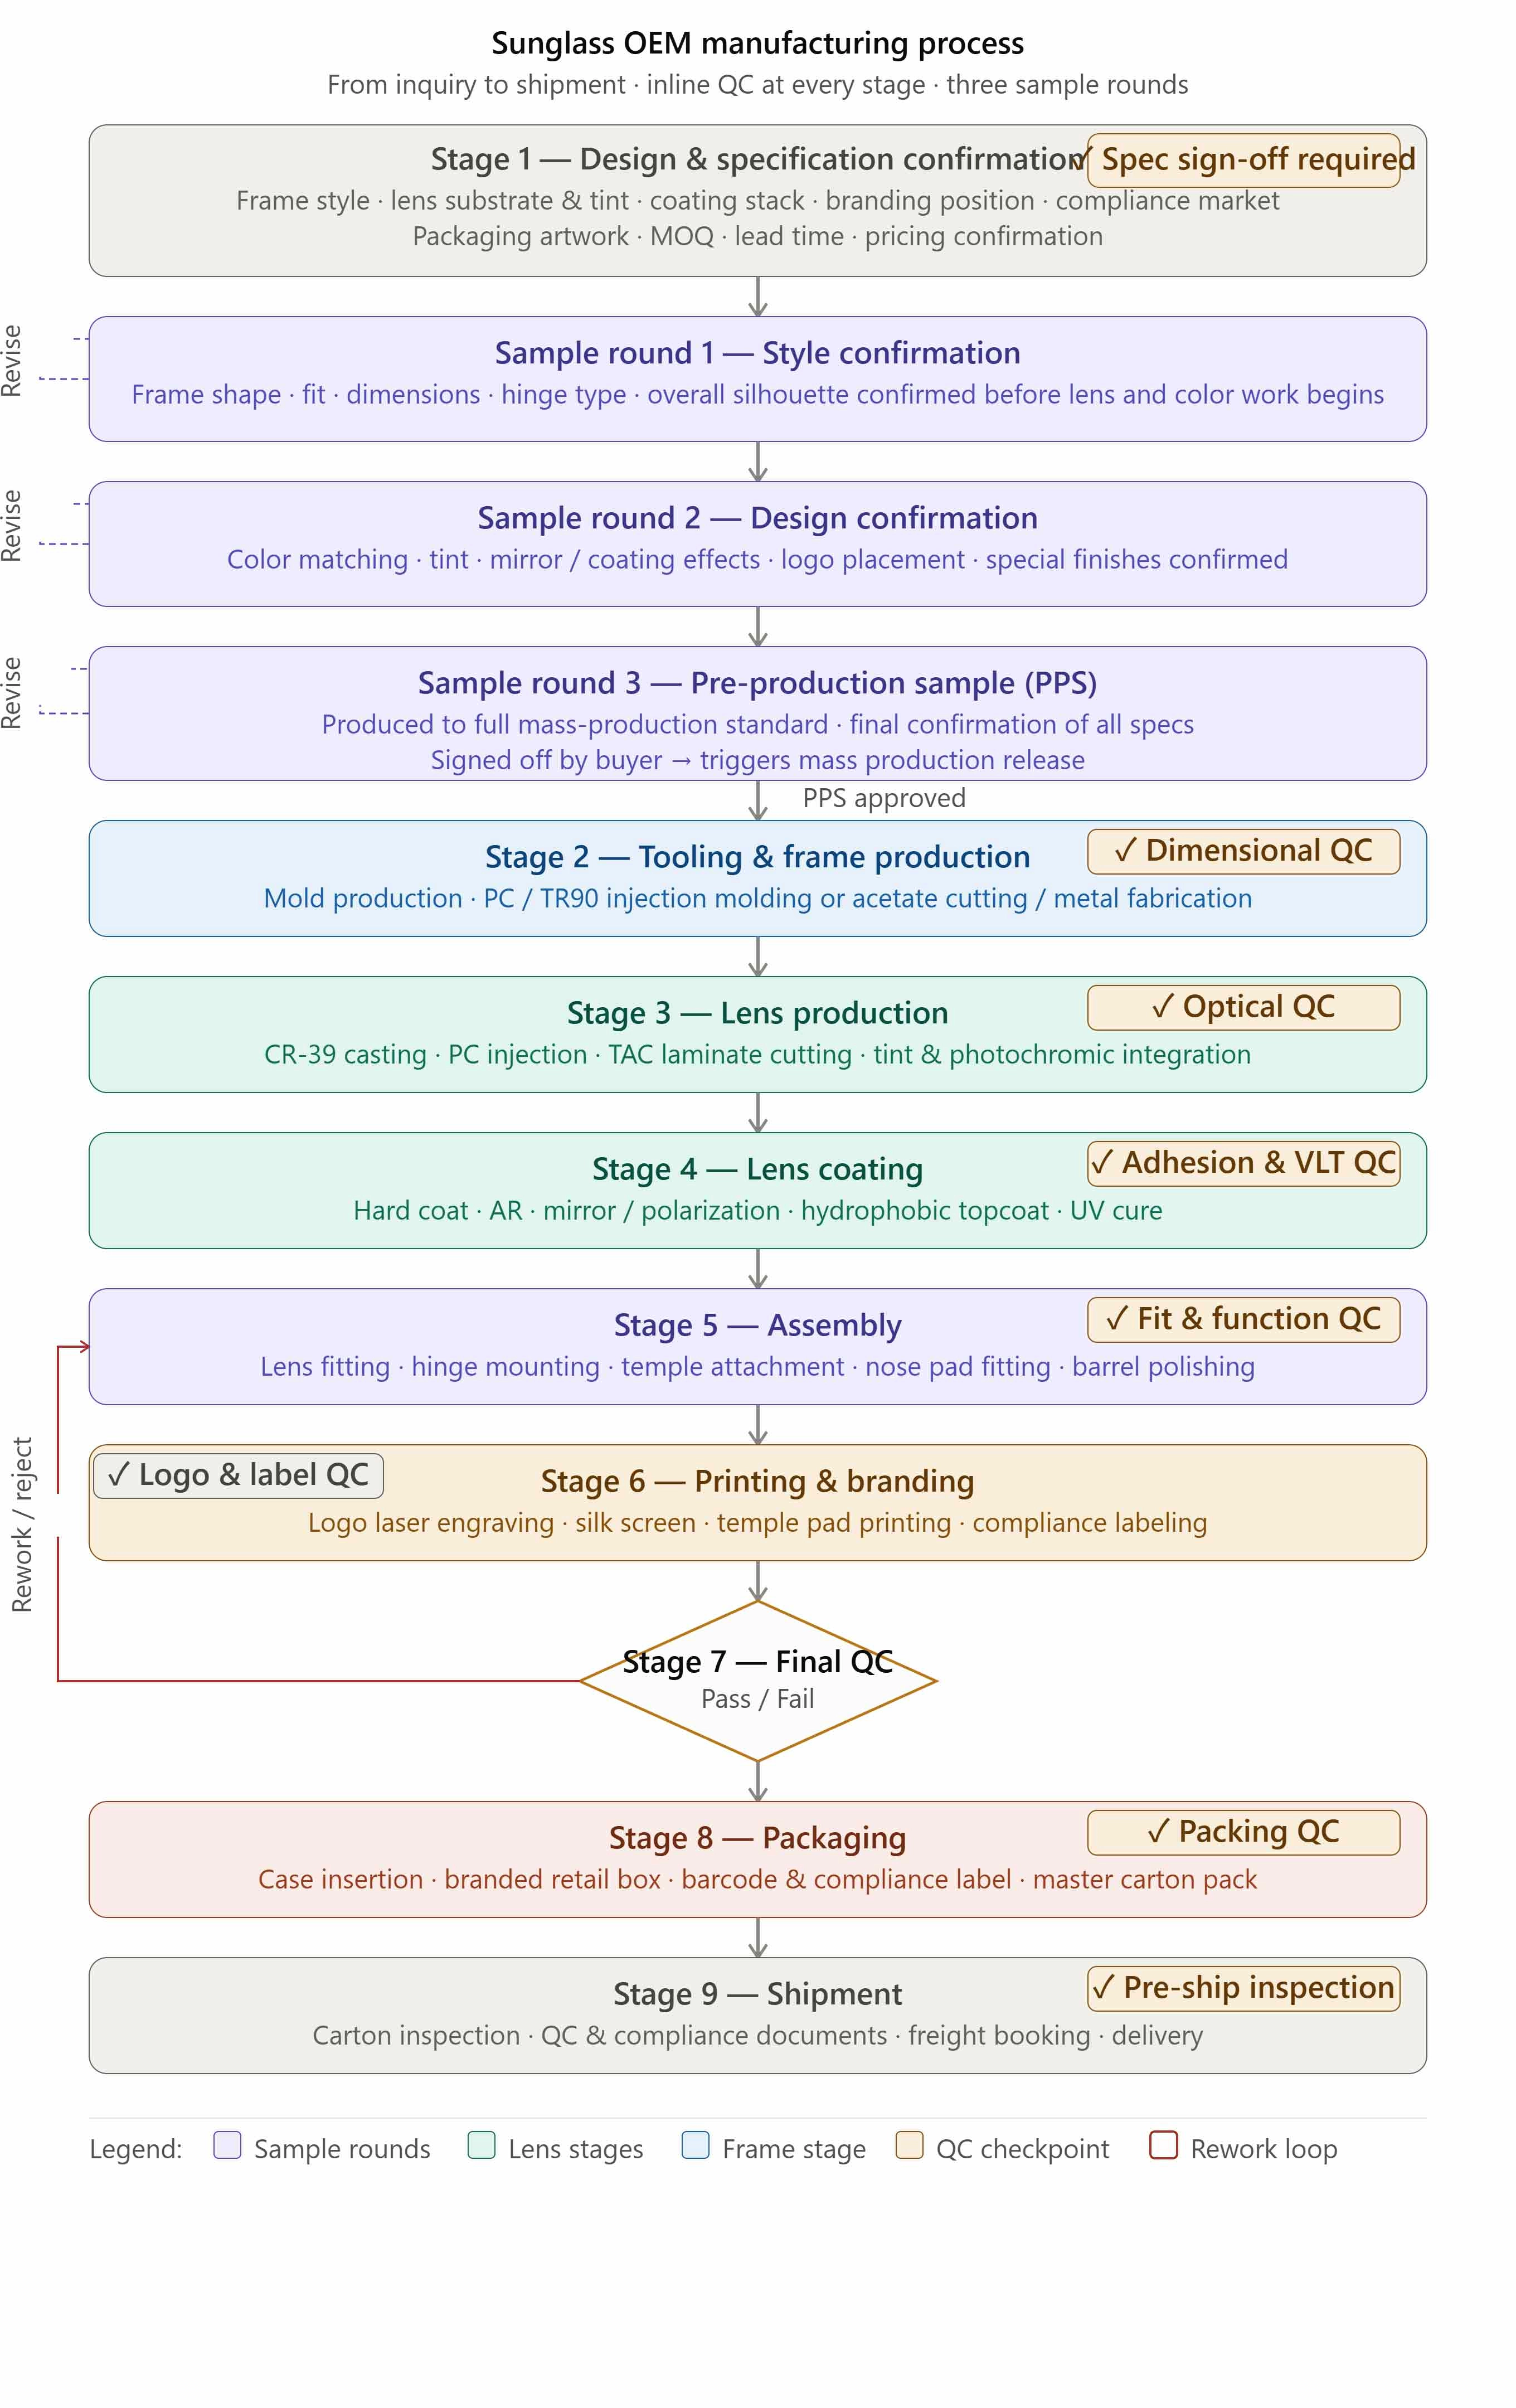
How Sunglasses Are Made: A Complete OEM Manufacturing Process Guide

Sunglass Lens Materials Compared: CR-39, PC, TAC, Nylon and Mineral Glass

Sunglass Lens Tint Categories Explained: A Complete Guide to Visible Light Transmittance for OEM Eyewear Brands

OEM Photochromic Lenses: Technology, Custom Options & B2B Sourcing Guide

Prescription Myopia Sunglass Lenses: Complete Guide on Optics, Production Process & Material Selection

Polarized Sunglasses with Anti-Seawater Coating: Technical OEM Specification Guide for Marine & Watersports Eyewear
You May Also Like
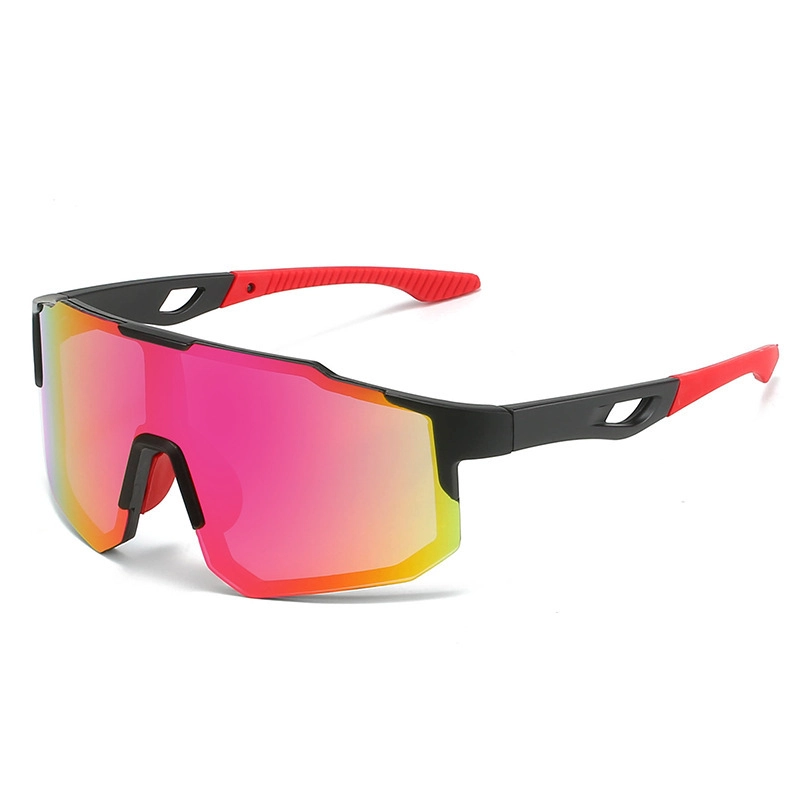
Wholesale Wraparound Sports Cycling Sunglasses, UV400 Impact‑Resistant Outdoor Goggles, Unisex Oversized One‑Piece Lens Shades
This wraparound sports cycling sunglasses features one‑piece oversized lens, ergonomic full‑wrap frame structure. Lightweight high‑toughness frame material, fitted soft textured nose pads and anti‑slip curved temple tips. Delivers UV400 sun protection and impact‑resistant performance. Multiple mirror‑coated lens & frame color options for men and women. Perfect inventory pick for sports shops, outdoor gear retailers, cross‑border sellers and brand partners. Support mixed‑color bulk order, logo engraving, neutral packing and full private‑label customization.
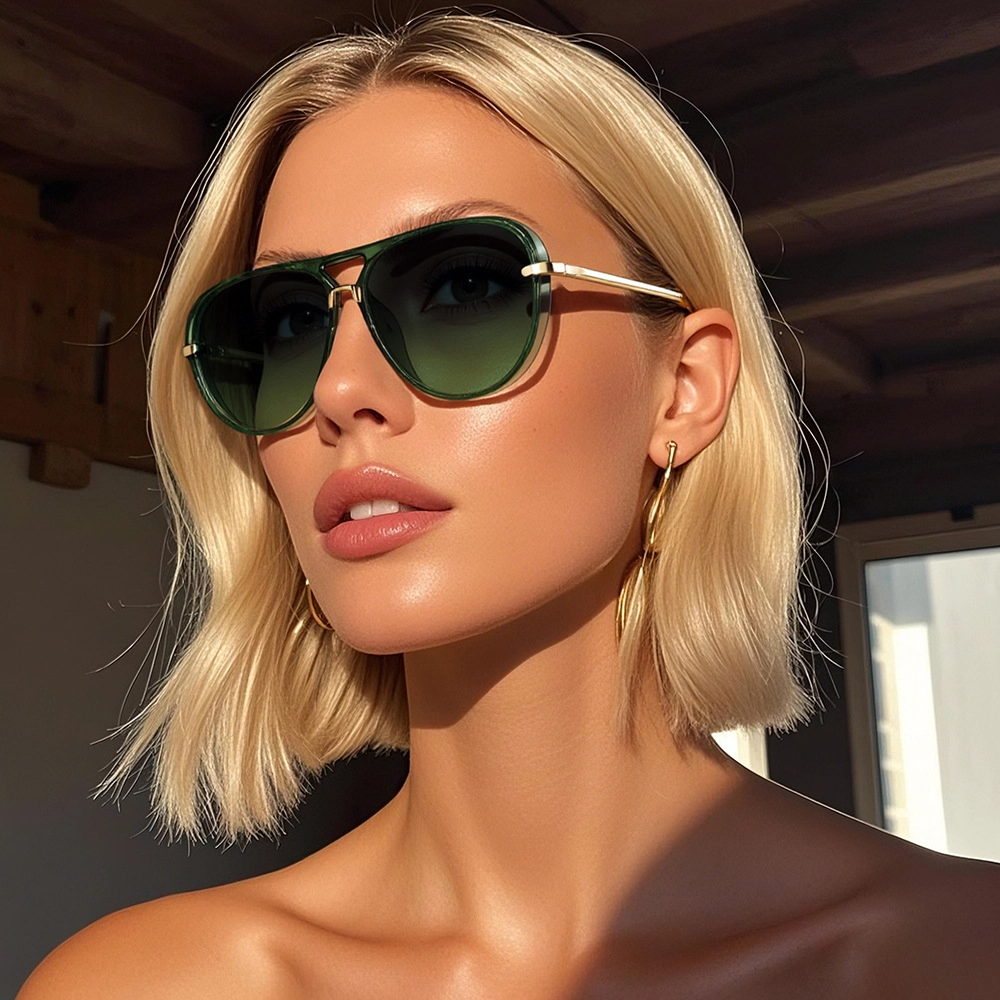
New Oversized Pilot Sunglasses for Women & Men – Retro Double-Bridge Aviator Sun Glasses, PC Frame, Fluorescent Green Gradient Lens, UV Protection
A bold, oversized take on the classic aviator. This double-bridge pilot frame pairs a wide PC front with slim gold-tone metal temples and a sculpted keyhole bridge for an elevated, editorial look. Offered in high-shine black, transparent amber, and the season's stand-out fluorescent green gradient. Lightweight at just 30.7 g, full UV protection, and a unisex fit that sells to both women's and men's channels. A strong add for boutiques, fashion accessories buyers, and online resellers chasing the current celebrity/influencer aviator trend.
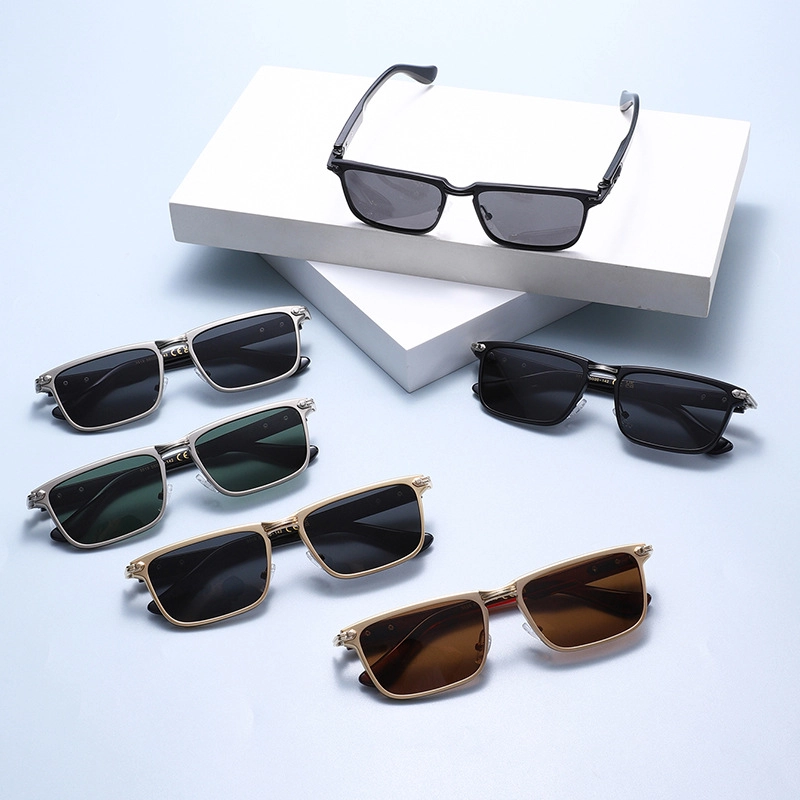
Wholesale Metal Square Polarized Sunglasses, Retro Sport Casual UV400 Sun Glasses Unisex Custom Logo Bulk for Physical Stores Distributors
Model KARMT008 is premium unisex metal square polarized sunglasses, blending retro styling with sport‑casual practicality. Sturdy full‑metal frame construction, multiple premium colorways in stock. Polarized UV400 lenses eliminate harsh glare for driving, outdoor sports and daily street wear.
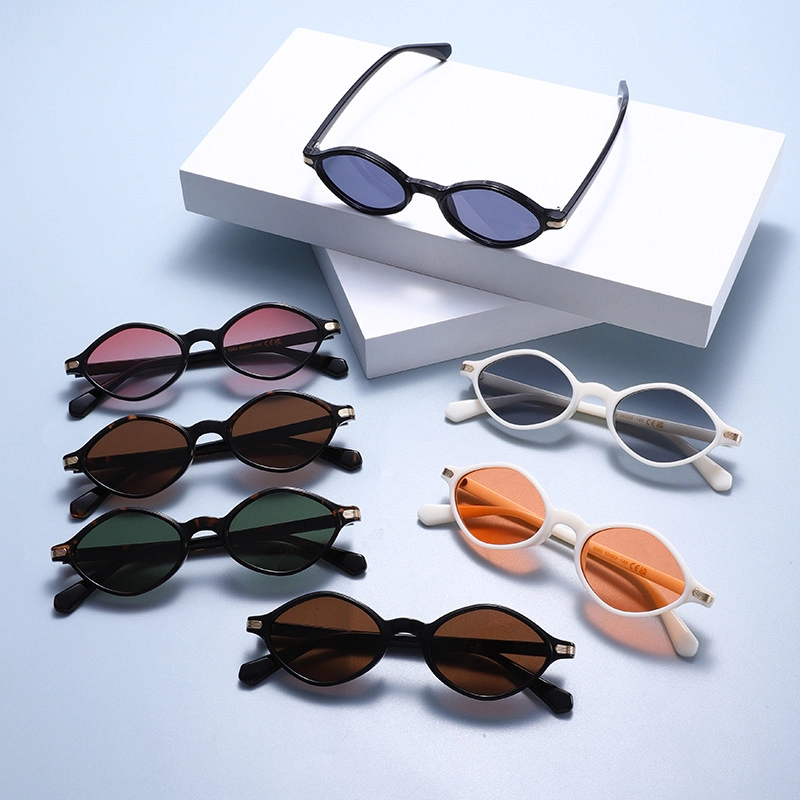
Wholesale Retro Oval Sunglasses, European American Style UV400 Unisex Fashion Sun Shades Custom Logo
Model KARPC017 is vintage European‑American style oval sunglasses. Classic compact oval silhouette accented with premium metal decorative details on temples. Light‑weight frame weighs only 21g, equipped with UV400 protective tint lenses. Multiple trendy ready‑stock colorways for men and women.
Perfect inventory option for physical eyewear boutiques, apparel stores, cross‑border e‑commerce sellers and brand owners. Support mixed‑color assortment, temple laser engraving, neutral packing and full private‑label customization.
Get in touch with us
If you have any comments or good suggestions, please leave us a message; later our professional staff will contact you as soon as possible.
NEW DIMENSIONS IN EYEWEAR
Contact KARUSON
Email:
WhatsApp/Phone:
Address:
331 Section B, WanJia Creative Park , No. 1 BUXIA Road ,Tianhe District, Guangzhou City, Guangdong Province, China.

© 2026 KARUSON. All Rights Reserved.
Facebook
Instagram
YouTube
TikTok
Linkedin