


How can eyewear factories customize TR sunglasses efficiently?
- 1. How can an eyewear factory reduce TR-90 frame tooling time from prototype to mass production under six weeks?
- 2. What practical steps can an eyewear factory take to ensure consistent Pantone color matching on TR sunglasses across injection batches?
- 3. How can an eyewear factory apply durable metal plating on TR-90 temples without adhesion failure and high reject rates?
- 4. How to integrate polarized lens assembly into a TR sunglasses production line to minimize lens-fit defects and maintain UV400 certification?
- 5. How can eyewear factories meet low MOQs for startups while keeping per-unit costs reasonable for TR sunglasses?
- 6. What QC protocols should an eyewear factory implement for TR sunglasses to reduce returns due to warping and plating flaking?
How Can Eyewear Factories Customize TR Sunglasses Efficiently?
As an experienced eyewear manufacturer and OEM supplier, this guide answers six specific, often-missed questions beginners ask when working with an eyewear factory on TR sunglasses. It embeds proven production controls, injection mold and tooling workflows, color and plating best practices, polarized lens assembly, MOQ strategies, and robust QC checks aligned with AQL and ISO approaches.
1. How can an eyewear factory reduce TR-90 frame tooling time from prototype to mass production under six weeks?
Pain point: Buyers need fast turnarounds for market windows but face long mold lead times and iterations.
Practical approach:
- Prioritize design for manufacturability (DFM) up front. A quick DFM review (24–72 hours) flags undercuts, thin walls, and draft issues that add tool iterations.
- Use rapid aluminum tooling for initial runs. Aluminum molds (soft tooling) allow 50–5,000 shots and can be finished in 7–14 days versus 4–8 weeks for hardened steel. For TR-90 frames aluminum tooling enables validation and small-volume sales while steel tooling is prepared in parallel.
- Employ 3D-printed prototypes and CNC-machined master patterns for verification before committing to injection molds. Combine a digital fit check with physical samples in 48–72 hours to reduce human revision cycles.
- Parallelize steps: order lenses, accessories, and packaging while tooling is finalized. This shortens overall lead time—procurement often dictates final delivery.
- Set a strict mold change control: freeze design after CMM-verified prototype approval. Use coordinate measuring machine (CMM) reports and sign-offs to prevent late changes that add weeks.
Typical timeline (industry practice): Rapid tooling + prototype approval: 1–3 weeks; hardened steel production mold: 3–6 weeks. Combined approach can yield validated small production in ~4–6 weeks depending on complexity.
2. What practical steps can an eyewear factory take to ensure consistent Pantone color matching on TR sunglasses across injection batches?
Pain point: Color drift between batches causes visible SKU inconsistencies, returns, and brand problems.
Best practices:
- Develop a color masterbatch and lock the formula. Use a verified masterbatch supplier and keep a lot-controlled stock for repeat runs.
- Use a spectrophotometer for objective color measurement (Delta E targets). Aim for Delta E ≤ 2 for highly visible consumer surfaces; document the acceptable threshold in the production spec.
- Compensate for shrinkage and post-mold gloss: TR-90 exhibits slight dimensional and surface gloss variation after cooling. Produce color compensation curves during pilot runs and capture them in the color recipe.
- Control processing parameters: mold temperature, injection pressure, and cycle time significantly affect final shade. Lock these parameters in the SOP and log them per batch.
- Perform first-article color approval (FAI) with signed colorimeter readings and physical swatches stored with batch records.
For brands: include Pantone codes but require a physical swatch approval. Digital Pantone alone is insufficient for TR injection processes.
3. How can an eyewear factory apply durable metal plating on TR-90 temples without adhesion failure and high reject rates?
Pain point: Buyers order metal-look finishes but experience flaking, peeling, or uneven coverage post-shipment.
Technical process steps:
- Choose the right surface pretreatment. TR-90 is a polyamide-based thermoplastic; it needs proper etching or plasma treatment to create a consistent surface for metallization.
- Select metallization method by design and budget: vacuum metallization is good for thin, decorative finishes; electroless plating (with a conductive intermediate) or copper-nickel-chrome electroplating gives thicker, more durable layers but requires additional pretreatments.
- Apply a conductive coating (e.g., palladium catalyst or conductive polymer) before electroplating if electroplating is required. For TR-90, an adhesion promoter layer is critical.
- Specify plating thickness and test it. Salt spray and adhesion tests (cross-hatch tape test) should be defined in the QA checklist. Typical decorative chrome finishes require a base copper layer, nickel, then chrome—each layer specified by microns to balance durability and flexibility.
- Control handling and bending during assembly. Over-flexing plated temples can cause micro-cracks; validate flex cycles per design (e.g., 5,000 flex cycles for hinges) and inspect post-test.
Quality metrics: set target pass rates for adhesion tests (e.g., ≥98%) and perform incoming plating batch audits; sample at AQL 2.5 for critical visual and adhesion checks.
4. How to integrate polarized lens assembly into a TR sunglasses production line to minimize lens-fit defects and maintain UV400 certification?
Pain point: Lens popping, misalignment, or failing UV standards lead to safety issues and costly recalls.
Integration checklist:
- Source certified polarized and UV400 lenses from qualified suppliers. Verify certificates of conformity stating UV400 compliance and polarization attenuation specs.
- Implement precise lens edging and CNC paddle systems. TR frames tolerances require lens edge shapes be exact; use CNC lens edgers and template verification to meet fit tolerances (±0.1 mm where critical).
- Use controlled adhesive dispensing or ultrasonic retention methods. For TR frames, ultrasonic welding or mechanical retention features (snap-in channels) are common to avoid visible glue lines; where adhesives are used, specify UV-stable, low-shrink adhesives and control bead volume with repeatable dispensing pumps.
- Perform functional checks: polarization axis verification (polarimeter), UV transmittance testing for UV400 compliance, and fit checks under light table to detect gaps or lens stress.
- Implement inline checks and end-of-line sampling under AQL 2.5 for lens placement, and 100% visual for safety critical dimensions if required by brand standards.
Document traceability: maintain lens lot numbers linked to frame batches in the ERP system for any field issues or recalls.
5. How can eyewear factories meet low MOQs for startups while keeping per-unit costs reasonable for TR sunglasses?
Pain point: Startups need market testing with small orders but face high per-unit cost and large mold commitments.
Strategies to lower entry barriers:
- Offer soft tooling or shared/multi-cavity molds. Factories often run shared molds where multiple brands produce small runs on one tool, reducing individual MOQ.
- Use modular components and standardized parts. Standard hinges, screws, and lenses reduce unique SKUs and allow mixing/matching to achieve lower MOQs.
- Negotiate phased tooling payments. Many manufacturers amortize tooling costs across subsequent orders or offer tooling-as-a-service where buyers pay a lower upfront fee.
- Leverage pre-production batches and reserved inventory. Commit to staggered purchases where the buyer pays a deposit to reserve capacity and spread cost over time.
- Consider print-on-demand finishing techniques such as pad printing or UV digital printing to avoid mold changes for small color runs.
Typical MOQ reality: for injection-molded TR frames a practical MOQ per color/style is often 300–1,000 pcs; however, with soft tooling or shared molds, MOQ can drop to 50–200 units per SKU depending on the factory model.
6. What QC protocols should an eyewear factory implement for TR sunglasses to reduce returns due to warping and plating flaking?
Pain point: High return rates from field lead to warranty costs and damaged brand reputation.
Recommended QC framework:
- Incoming raw material checks: verify resin certificates, masterbatch lot numbers, and lens certificates; use material test reports (MTRs) to confirm polymer grade and additives.
- In-process control points: set hold points at first shot, mid-run, and end-run to check dimensions, color, gloss, and fit. Log machine parameters and operator sign-off to the batch record.
- Define acceptance levels using AQL sampling plans. For critical cosmetic issues (plating, frame finish), use stricter AQL (e.g., 0.65 or 1.0); for functional checks, consider 100% inspection for first runs.
- Environmental and mechanical testing: thermal cycling to simulate warping risk, 5,000 open/close hinge cycles, salt-spray for plated surfaces, and drop tests per brand requirements.
- Packaging and transport validation: ensure frames are blocked and padded to prevent plating abrasion. Define pack orientation and shock thresholds; run a distribution simulation if exporting internationally.
- Traceability and corrective action: implement batch codes, nonconformance reports (NCRs), and CAPA (corrective and preventive action) logs tied to suppliers and machine IDs.
Compliance references: many factories follow ISO 9001 frameworks for quality management; use AQL 2.5 or stricter for consumer eyewear quality assurance.
Conclusion: Partnering with a professional eyewear factory that understands TR-90 frames, injection mold workflows, plating science, polarized lens assembly, and low-MOQ strategies yields faster market entry, stable brand colors, durable finishes, and reduced returns. A structured roadmap—DFM, rapid tooling, masterbatch control, proper metallization pretreatment, certified lens sourcing, and robust QC (AQL, environmental and mechanical tests)—is the industry-standard path to efficient TR sunglasses customization.
Advantages of working with a specialized eyewear manufacturer include reduced lead times through rapid tooling, predictable color and finish control, scalable production from small to large volumes, integrated polarized lens assembly, and documented QC that protects brand reputation.
Contact us for a quote: visit www.karusonco.com or email nicole@karusonco.com.
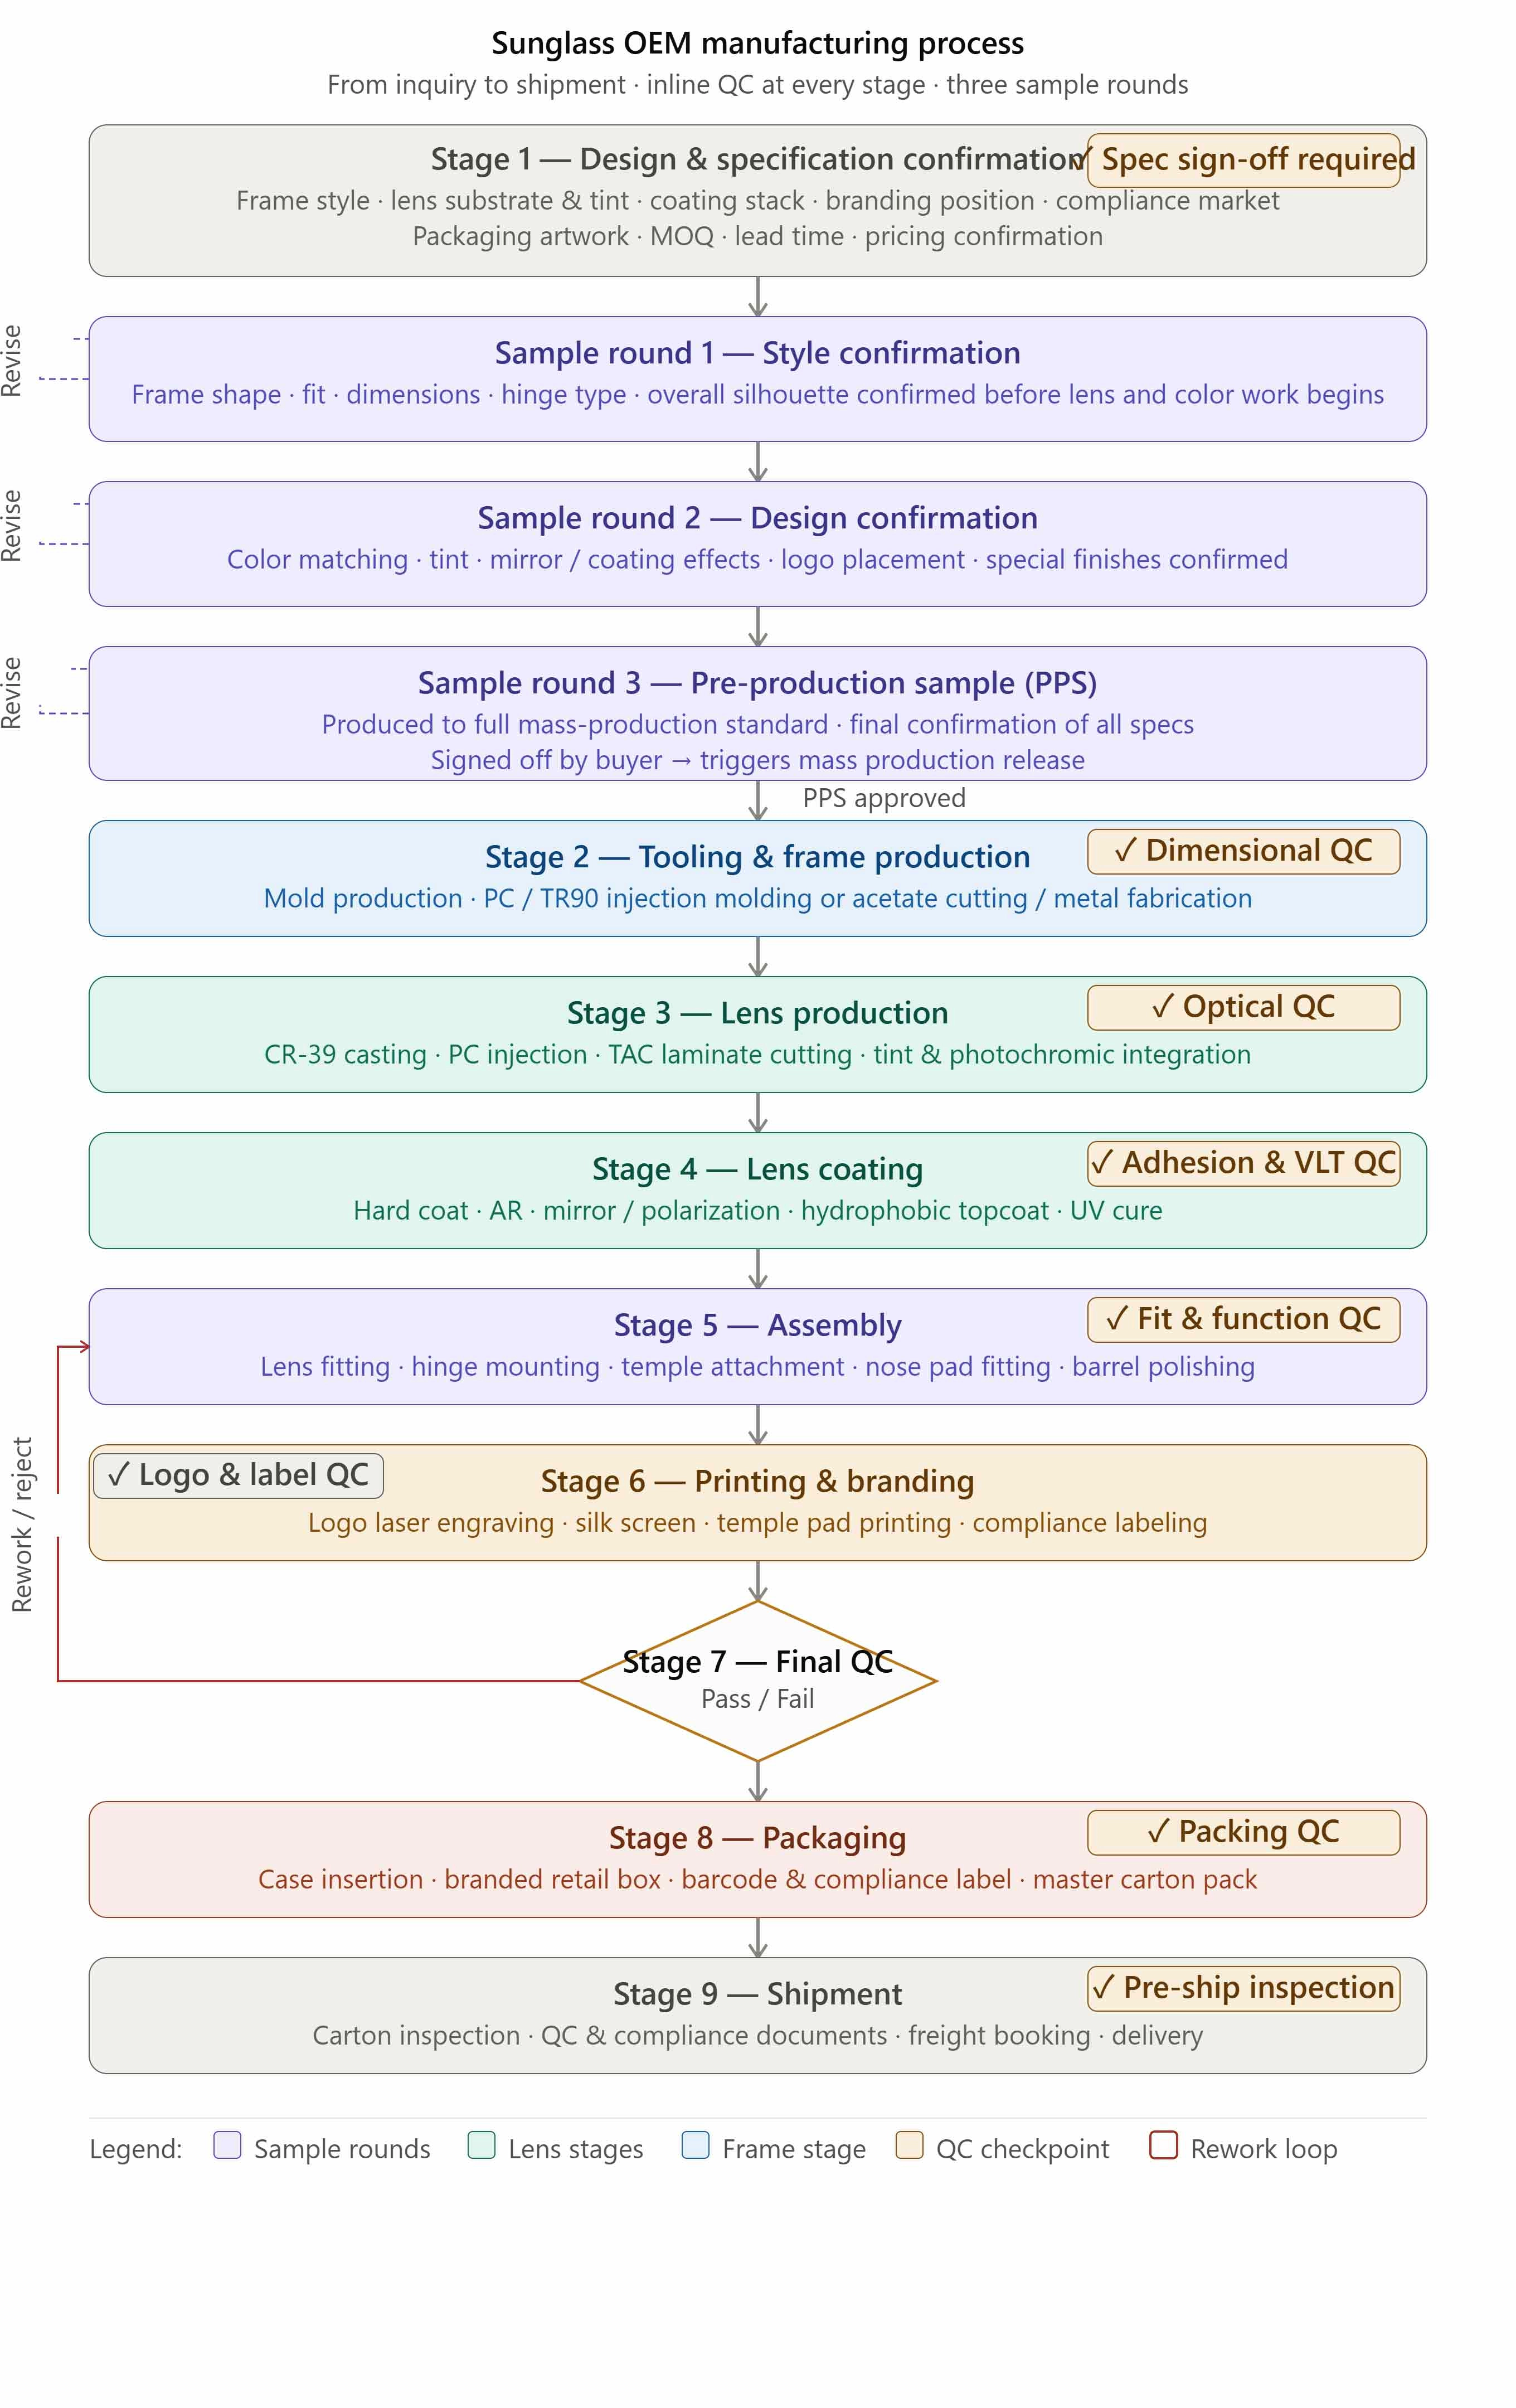
How Sunglasses Are Made: A Complete OEM Manufacturing Process Guide

Sunglass Lens Materials Compared: CR-39, PC, TAC, Nylon and Mineral Glass

Sunglass Lens Tint Categories Explained: A Complete Guide to Visible Light Transmittance for OEM Eyewear Brands

OEM Photochromic Lenses: Technology, Custom Options & B2B Sourcing Guide

Prescription Myopia Sunglass Lenses: Complete Guide on Optics, Production Process & Material Selection

Polarized Sunglasses with Anti-Seawater Coating: Technical OEM Specification Guide for Marine & Watersports Eyewear
You May Also Like
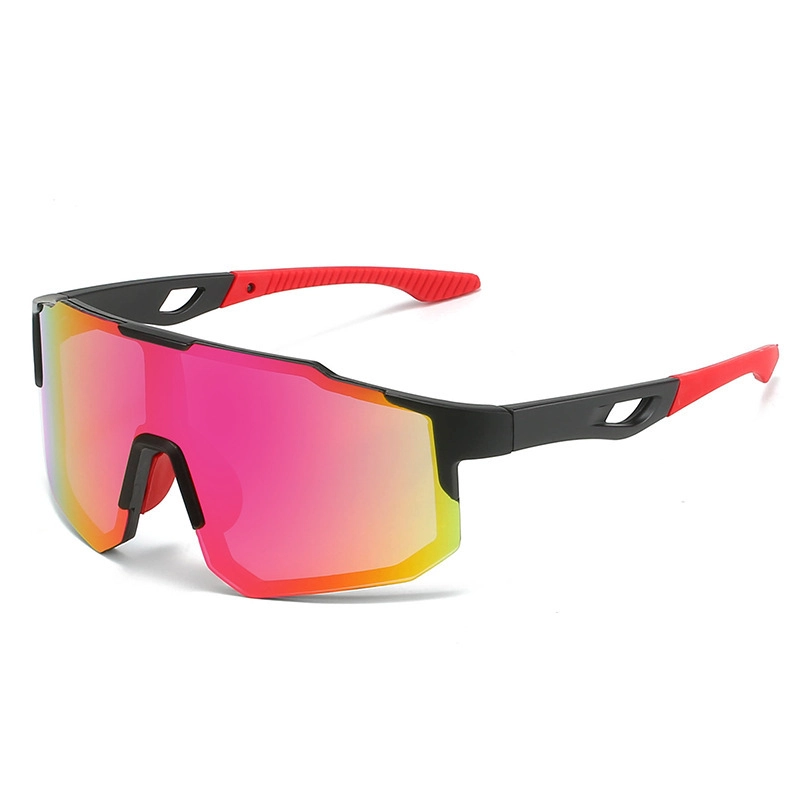
Wholesale Wraparound Sports Cycling Sunglasses, UV400 Impact‑Resistant Outdoor Goggles, Unisex Oversized One‑Piece Lens Shades
This wraparound sports cycling sunglasses features one‑piece oversized lens, ergonomic full‑wrap frame structure. Lightweight high‑toughness frame material, fitted soft textured nose pads and anti‑slip curved temple tips. Delivers UV400 sun protection and impact‑resistant performance. Multiple mirror‑coated lens & frame color options for men and women. Perfect inventory pick for sports shops, outdoor gear retailers, cross‑border sellers and brand partners. Support mixed‑color bulk order, logo engraving, neutral packing and full private‑label customization.
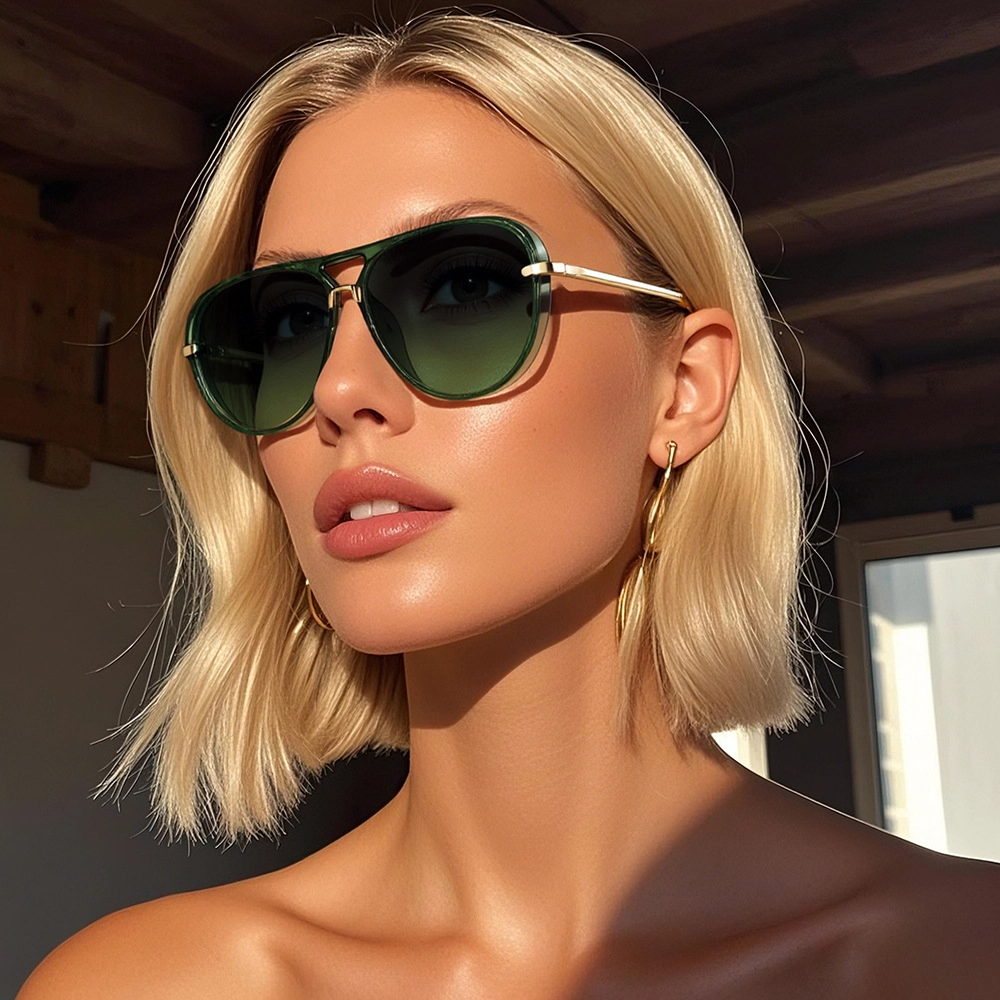
New Oversized Pilot Sunglasses for Women & Men – Retro Double-Bridge Aviator Sun Glasses, PC Frame, Fluorescent Green Gradient Lens, UV Protection
A bold, oversized take on the classic aviator. This double-bridge pilot frame pairs a wide PC front with slim gold-tone metal temples and a sculpted keyhole bridge for an elevated, editorial look. Offered in high-shine black, transparent amber, and the season's stand-out fluorescent green gradient. Lightweight at just 30.7 g, full UV protection, and a unisex fit that sells to both women's and men's channels. A strong add for boutiques, fashion accessories buyers, and online resellers chasing the current celebrity/influencer aviator trend.
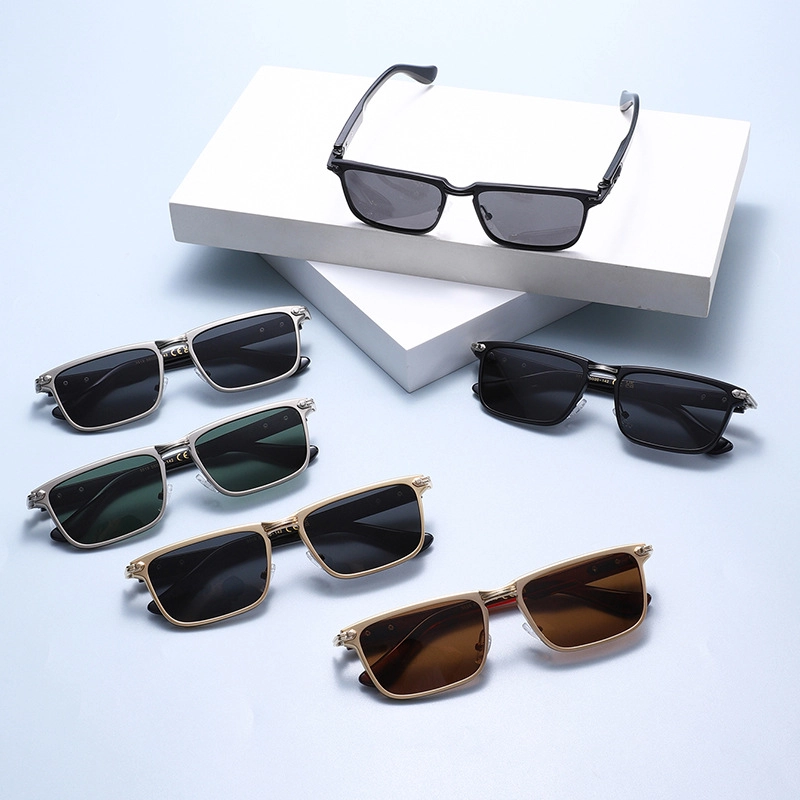
Wholesale Metal Square Polarized Sunglasses, Retro Sport Casual UV400 Sun Glasses Unisex Custom Logo Bulk for Physical Stores Distributors
Model KARMT008 is premium unisex metal square polarized sunglasses, blending retro styling with sport‑casual practicality. Sturdy full‑metal frame construction, multiple premium colorways in stock. Polarized UV400 lenses eliminate harsh glare for driving, outdoor sports and daily street wear.
Wholesale Retro Oval Sunglasses, European American Style UV400 Unisex Fashion Sun Shades Custom Logo
Model KARPC017 is vintage European‑American style oval sunglasses. Classic compact oval silhouette accented with premium metal decorative details on temples. Light‑weight frame weighs only 21g, equipped with UV400 protective tint lenses. Multiple trendy ready‑stock colorways for men and women.
Perfect inventory option for physical eyewear boutiques, apparel stores, cross‑border e‑commerce sellers and brand owners. Support mixed‑color assortment, temple laser engraving, neutral packing and full private‑label customization.
Get in touch with us
If you have any comments or good suggestions, please leave us a message; later our professional staff will contact you as soon as possible.
NEW DIMENSIONS IN EYEWEAR
Contact KARUSON
Email:
WhatsApp/Phone:
Address:
331 Section B, WanJia Creative Park , No. 1 BUXIA Road ,Tianhe District, Guangzhou City, Guangdong Province, China.

© 2026 KARUSON. All Rights Reserved.
Facebook
Instagram
YouTube
TikTok
Linkedin