


Can metal sunglasses be electroplated or coated reliably?
- Can metal sunglasses be electroplated for durable consumer use?
- Which metal substrates in eyewear factory accept plating best?
- How to control adhesion and prevent flaking on frames?
- Are PVD coatings better than electroplating for corrosion resistance?
- What environmental and regulatory limits affect plating in factories?
- How to test coating durability and colorfastness in production?
Can metal sunglasses be electroplated or coated reliably?
Reliable metal finishes for sunglasses are achievable when the correct substrate preparation, chemistry, and quality controls are applied; this article distills production-proven methods, limits of common metals, alternatives like PVD, and test protocols used by eyewear factory operations to ensure durability and compliance.
Can metal sunglasses be electroplated for durable consumer use?
Yes, electroplating can produce durable consumer-grade finishes when engineered for the intended wear profile. Decorative chrome over a nickel underlayer remains common for aesthetics and abrasion resistance, but durability depends on proper pre-treatment, deposition sequence, and layer thickness control. For production in an eyewear factory, a multi-stage line is typical: degrease, mechanical/chemical surface activation, strike layer to promote adhesion, bulk deposit, and final seal or topcoat. Process control metrics to track include bath chemistry (metal ion concentration and pH), current density uniformity across frames, and plating thickness tolerances. Electroplated finishes are vulnerable to edge flaking if blind corners and internal bore areas are not addressed by racking design and optimized current distribution, so tooling and electrical contact planning are integral to real-world longevity.
Which metal substrates in eyewear factory accept plating best?
The ease of plating is substrate specific. Copper, brass, and standard low-alloy steels accept traditional electroplating readily after simple cleaning. Aluminum requires a zincate pre-treatment to remove the oxide and provide a receptive surface. Stainless steel and titanium are more challenging: stainless needs aggressive activation and often a nickel strike or electroless nickel preplate to achieve adhesion, while titanium typically resists direct electroplating because of a stable oxide layer and often receives PVD or electroless nickel after specialized surface activation. Understanding substrate behavior is essential for an eyewear factory because material selection drives downstream finishing choices and cost of process qualification.
How to control adhesion and prevent flaking on frames?
Adhesion failures are most often rooted in inadequate surface preparation, improper rack contact, or insufficient intermediate layers. Best practices include precision cleaning (solvent and alkaline stages), micro-etch or light abrasive blasting to remove mill scale, followed by a chemical activation and a strike layer that bonds to both substrate and bulk deposit. Electroless nickel as an intermediate layer is widely used for its conformal coverage and corrosion barrier properties. Statistical process control for bath contaminants, regular destructive cross-section analysis, and routine adhesion testing such as an ASTM D3359 cross hatch or tape test help detect problems early. Mechanical design matters too: sharp edges should be radiused, and plating fixtures must avoid insulated islands that cause localized underplating and subsequent flaking.
Are PVD coatings better than electroplating for corrosion resistance?
PVD and electroplating solve different problems and can be complementary. PVD produces very adherent, thin hard films with superior wear resistance and a growing set of decorative finishes including gold tones, gunmetal, and black titanium nitride. PVD is often preferred when plating on difficult substrates such as titanium or when hexavalent chromium restrictions apply. Electroplating with nickel and chromium can provide excellent corrosion protection when layer thicknesses and seals are correct. In many eyewear factory applications, electroless nickel plus PVD topcoat or PVD over a plated barrier combines the galvanic and barrier protection of plating with the hardness and color stability of PVD. Selection should be based on required wear cycles, salt spray targets, and cost per part under production volumes.
What environmental and regulatory limits affect plating in factories?
Regulatory constraints shape finishing choices. Hexavalent chromium use is restricted or banned in many jurisdictions, driving suppliers to trivalent chromium chemistries or non-chrome alternatives like PVD. Wastewater containing heavy metals such as nickel, copper, and zinc requires treatment to meet local discharge limits and may trigger permits from agencies such as the US EPA or equivalent regional authorities. Restrictions under REACH and RoHS also influence alloying and plating chemistries. An eyewear factory must invest in proper effluent treatment, chemical substitution assessments, and compliance documentation to avoid fines and production interruptions; lifecycle and end-of-sale country compliance must be validated during product specification and supplier selection.
How to test coating durability and colorfastness in production?
Standardized testing protects against field failures. Corrosion testing commonly uses neutral salt spray per ASTM B117 to establish relative resistance; 100 to 500 hours is a typical qualification window for consumer eyewear targets depending on finish class. Adhesion testing via cross hatch and tape tests per ASTM D3359, wear abrasion using Taber abrasion per ASTM D4060, and accelerated UV exposure using QUV or ASTM G154 are industry-accepted methods to verify finishing performance. In-line non-destructive checks such as coating thickness gauges and gloss/color spectrophotometry enable lot-level quality control, while periodic destructive cross-sections confirm interlayer integrity and true thickness. Implementing a testing matrix keyed to sales regions and end-use conditions ensures a controlled, repeatable finish process for an eyewear factory supply chain.
Conclusion: KARUSON brings hands-on finishing engineering, tooling know-how, and production-proven quality systems to resolve plating adhesion, substrate compatibility, environmental compliance, and test protocol gaps that commonly undermine metal sunglasses finishing in contract manufacturing environments.
Contact us for a production quote at www.karusonco.com or email nicole@karusonco.com.
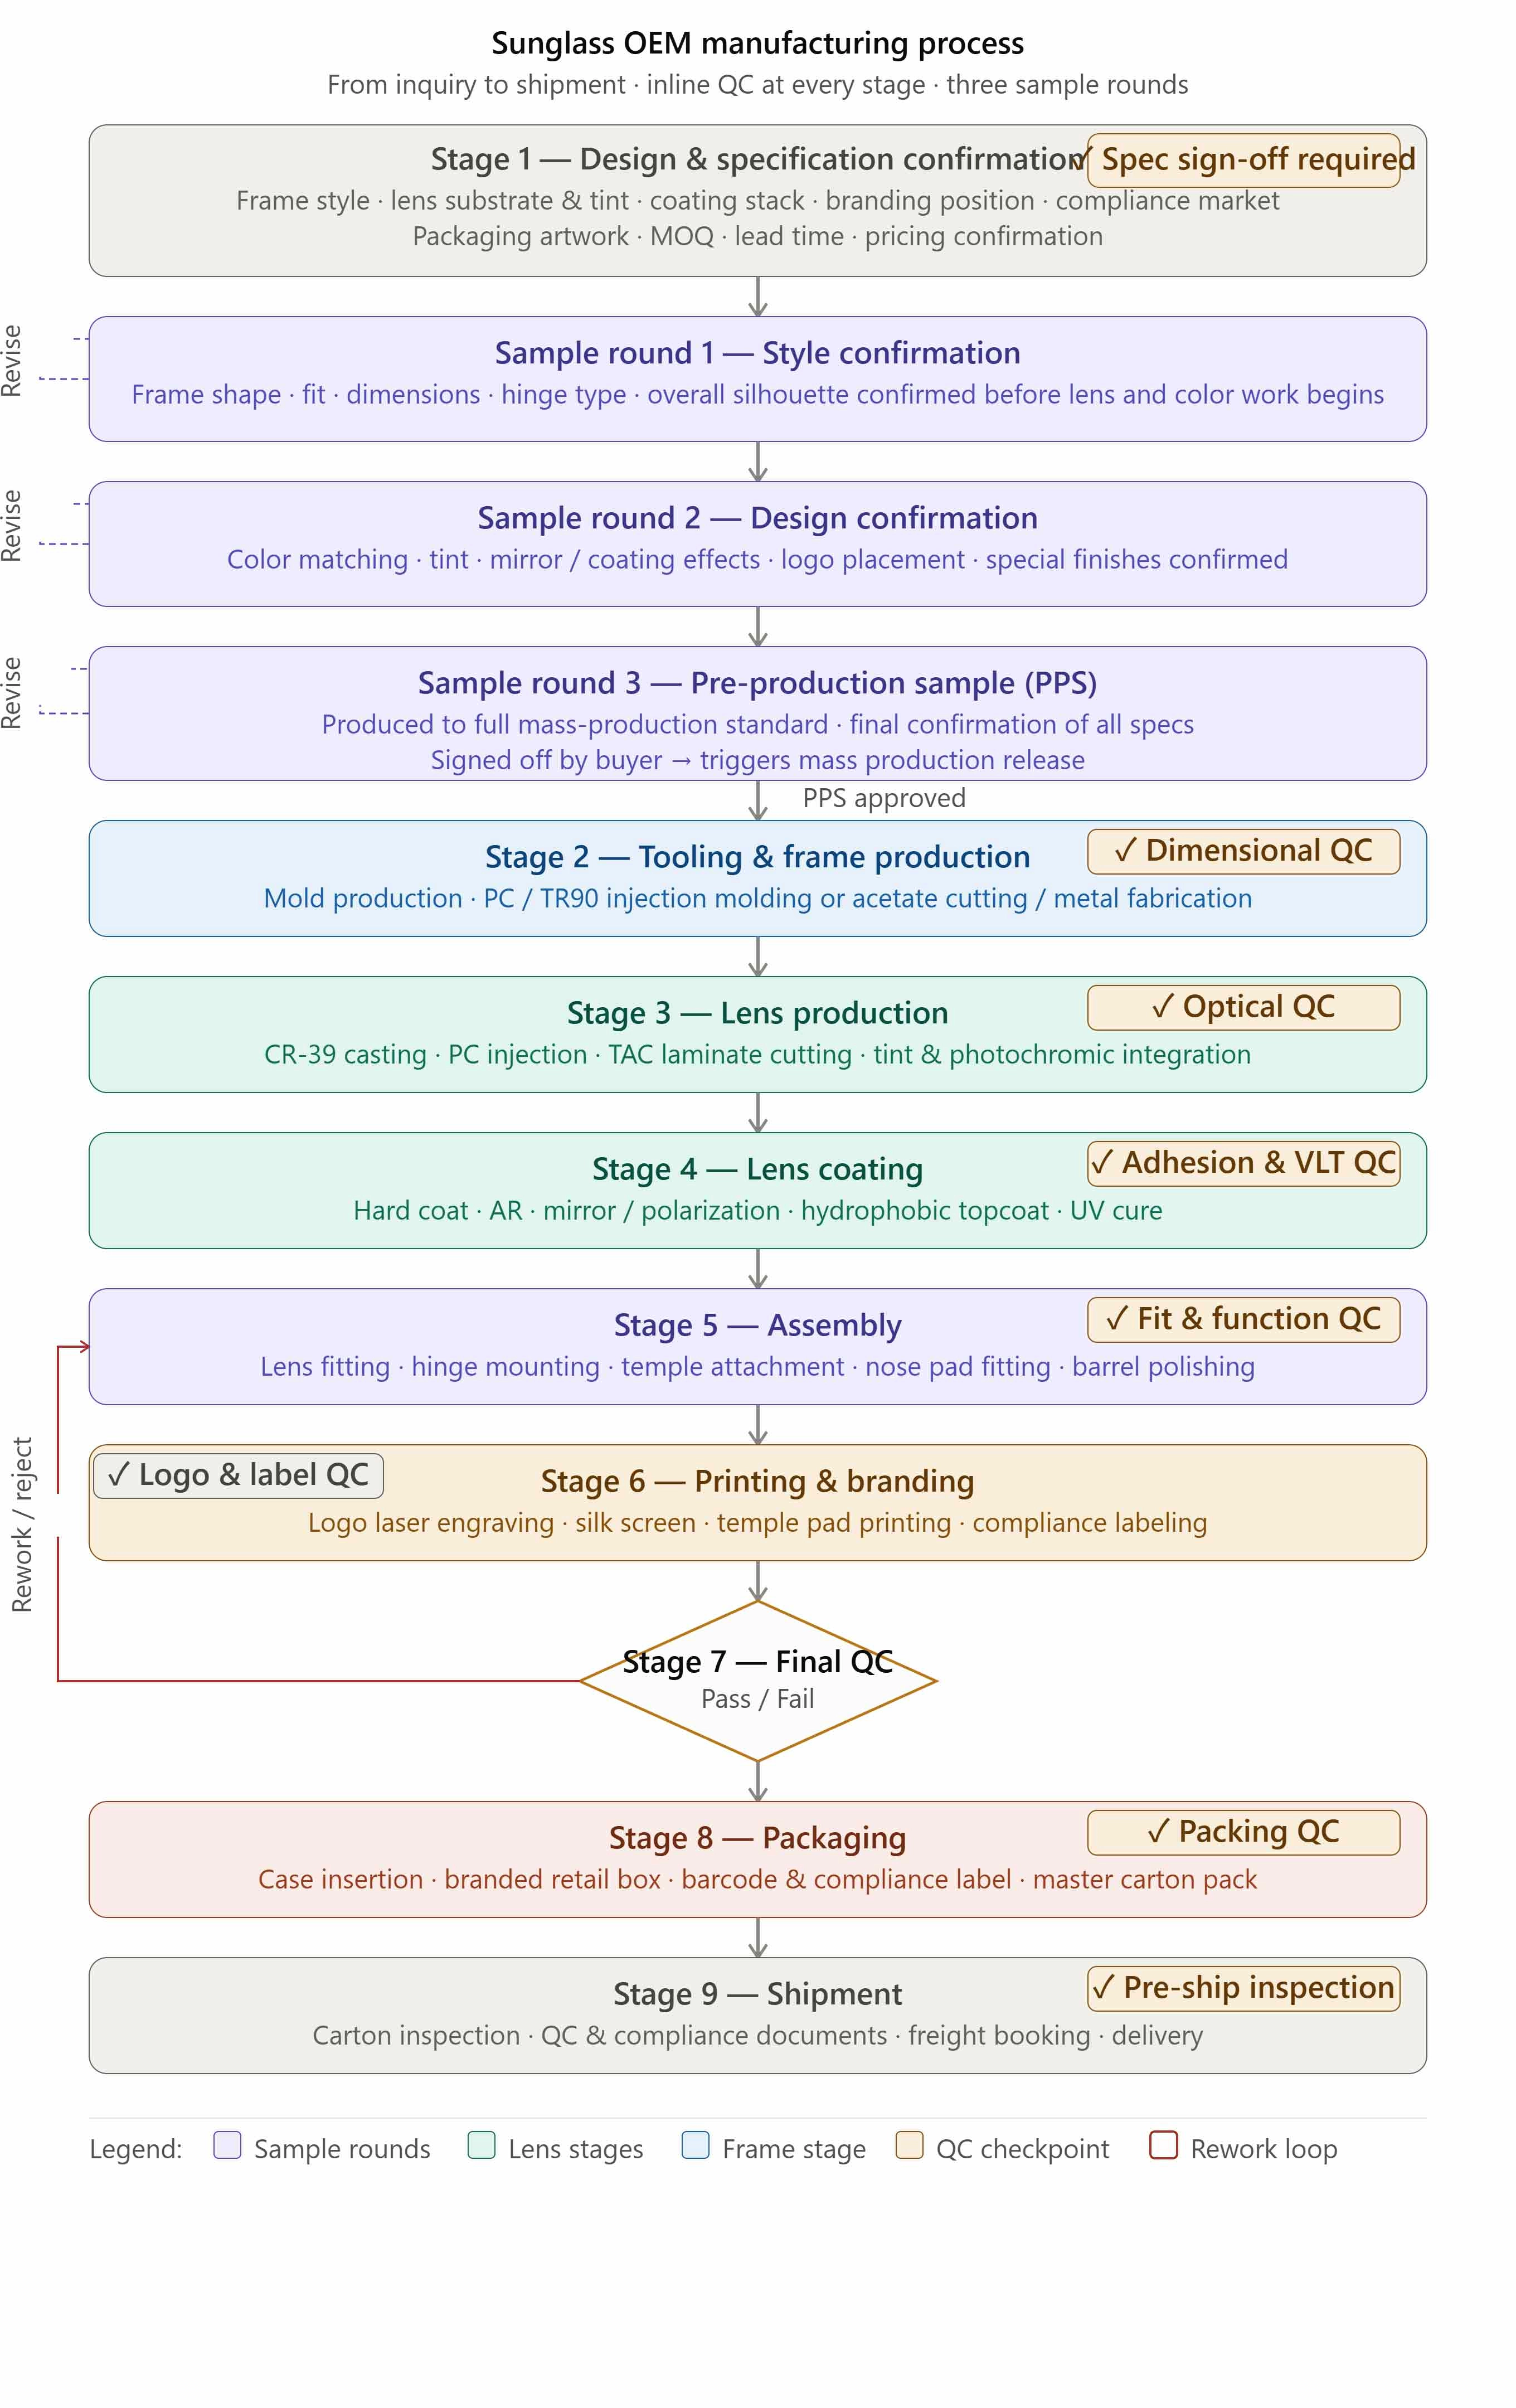
How Sunglasses Are Made: A Complete OEM Manufacturing Process Guide

Sunglass Lens Materials Compared: CR-39, PC, TAC, Nylon and Mineral Glass

Sunglass Lens Tint Categories Explained: A Complete Guide to Visible Light Transmittance for OEM Eyewear Brands

OEM Photochromic Lenses: Technology, Custom Options & B2B Sourcing Guide

Prescription Myopia Sunglass Lenses: Complete Guide on Optics, Production Process & Material Selection

Polarized Sunglasses with Anti-Seawater Coating: Technical OEM Specification Guide for Marine & Watersports Eyewear
You May Also Like
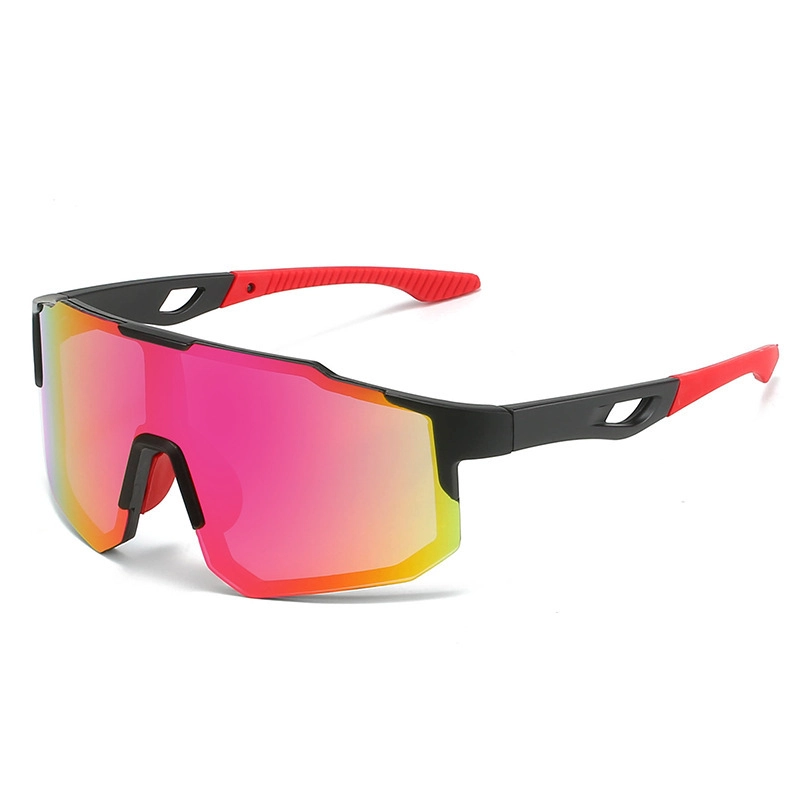
Wholesale Wraparound Sports Cycling Sunglasses, UV400 Impact‑Resistant Outdoor Goggles, Unisex Oversized One‑Piece Lens Shades
This wraparound sports cycling sunglasses features one‑piece oversized lens, ergonomic full‑wrap frame structure. Lightweight high‑toughness frame material, fitted soft textured nose pads and anti‑slip curved temple tips. Delivers UV400 sun protection and impact‑resistant performance. Multiple mirror‑coated lens & frame color options for men and women. Perfect inventory pick for sports shops, outdoor gear retailers, cross‑border sellers and brand partners. Support mixed‑color bulk order, logo engraving, neutral packing and full private‑label customization.
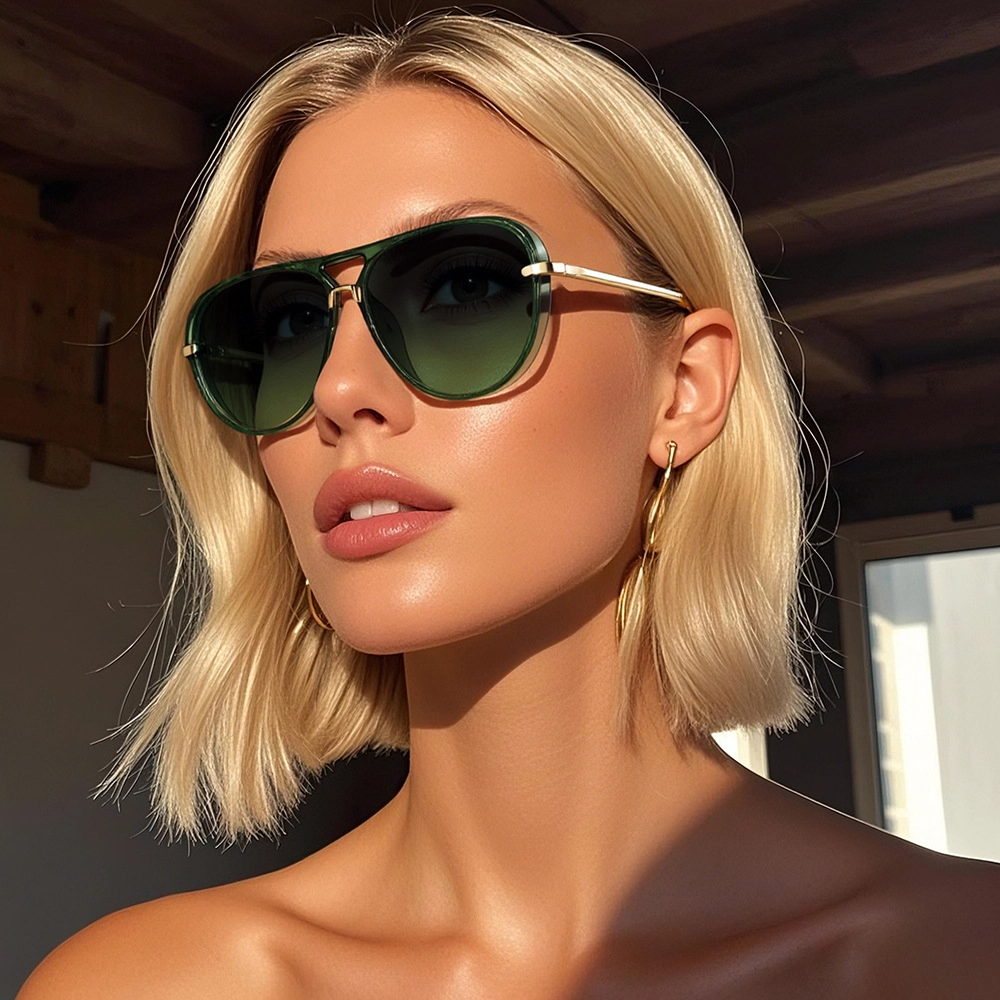
New Oversized Pilot Sunglasses for Women & Men – Retro Double-Bridge Aviator Sun Glasses, PC Frame, Fluorescent Green Gradient Lens, UV Protection
A bold, oversized take on the classic aviator. This double-bridge pilot frame pairs a wide PC front with slim gold-tone metal temples and a sculpted keyhole bridge for an elevated, editorial look. Offered in high-shine black, transparent amber, and the season's stand-out fluorescent green gradient. Lightweight at just 30.7 g, full UV protection, and a unisex fit that sells to both women's and men's channels. A strong add for boutiques, fashion accessories buyers, and online resellers chasing the current celebrity/influencer aviator trend.
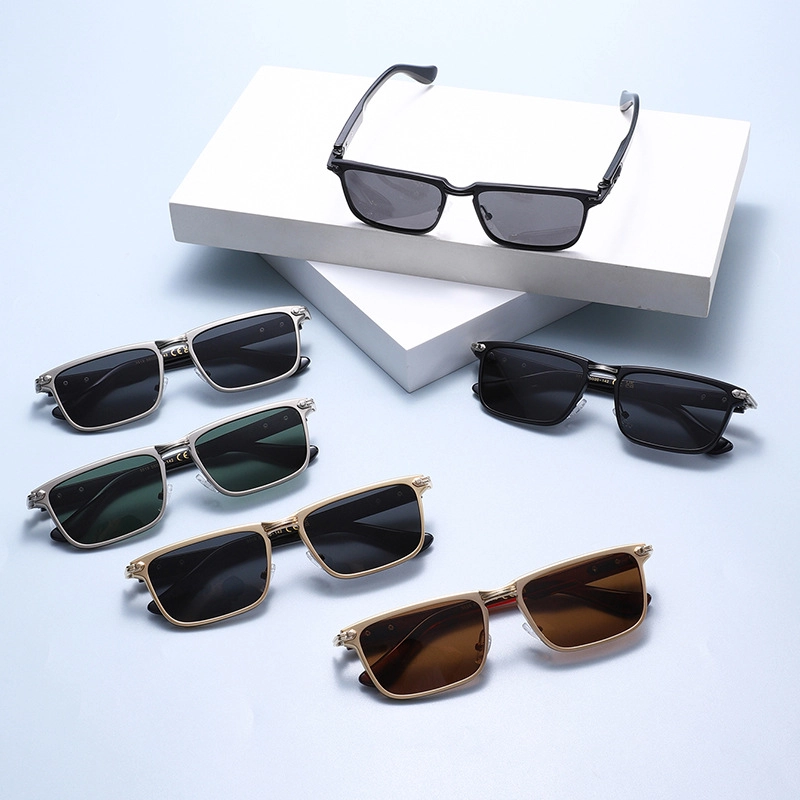
Wholesale Metal Square Polarized Sunglasses, Retro Sport Casual UV400 Sun Glasses Unisex Custom Logo Bulk for Physical Stores Distributors
Model KARMT008 is premium unisex metal square polarized sunglasses, blending retro styling with sport‑casual practicality. Sturdy full‑metal frame construction, multiple premium colorways in stock. Polarized UV400 lenses eliminate harsh glare for driving, outdoor sports and daily street wear.
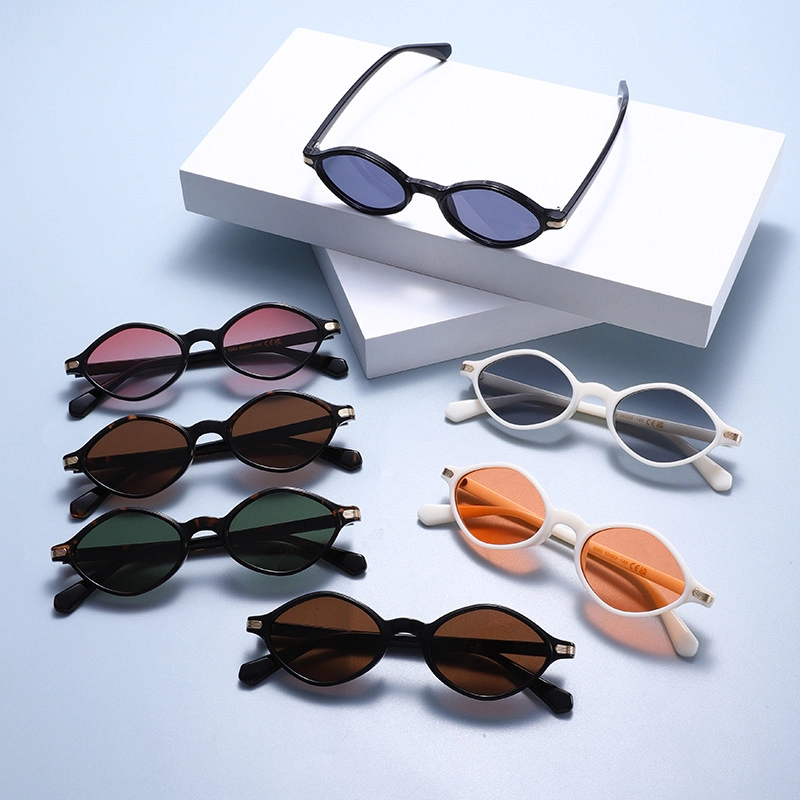
Wholesale Retro Oval Sunglasses, European American Style UV400 Unisex Fashion Sun Shades Custom Logo
Model KARPC017 is vintage European‑American style oval sunglasses. Classic compact oval silhouette accented with premium metal decorative details on temples. Light‑weight frame weighs only 21g, equipped with UV400 protective tint lenses. Multiple trendy ready‑stock colorways for men and women.
Perfect inventory option for physical eyewear boutiques, apparel stores, cross‑border e‑commerce sellers and brand owners. Support mixed‑color assortment, temple laser engraving, neutral packing and full private‑label customization.
Get in touch with us
If you have any comments or good suggestions, please leave us a message; later our professional staff will contact you as soon as possible.
NEW DIMENSIONS IN EYEWEAR
Contact KARUSON
Email:
WhatsApp/Phone:
Address:
331 Section B, WanJia Creative Park , No. 1 BUXIA Road ,Tianhe District, Guangzhou City, Guangdong Province, China.

© 2026 KARUSON. All Rights Reserved.
Facebook
Instagram
YouTube
TikTok
Linkedin