


How are TR sunglasses manufactured in modern eyewear factories?
- 1. How do modern eyewear factories control dimensional tolerances and warpage for TR-90 frames to ensure uniform lens fit across large production runs?
- 2. What injection molding parameters and mold maintenance practices reduce sink marks, flashing and short shots on TR sunglasses frames?
- 3. How do factories ensure coating adhesion and color consistency on TR-90 frames during mass finishing, plating or painting?
- 4. What QC tests and pass/fail criteria should buyers require for TR sunglasses to meet ISO 12312-1 and industry optical safety requirements?
- 5. How do modern factories perform lens edging and snap-in tolerance control for polarized and coated lenses to prevent micro-scratches and frame strain?
- 6. What logistics, MOQ, lead-time and tooling cost breakdown should buyers expect when ordering custom TR sunglasses from an eyewear factory?
- Concluding summary: Advantages of sourcing TR sunglasses from modern eyewear factories
How Are TR Sunglasses Manufactured in Modern Eyewear Factories?
This article answers six specific, under-documented questions beginners and industry buyers ask when sourcing TR sunglasses from an eyewear factory. It includes practical production steps, test criteria, acceptance tolerances and supplier negotiation points. Semantic keywords embedded: TR-90 frames, injection molding, ultrasonic welding, polarized lenses, CNC milling, anti-scratch coating, ISO 12312-1, tooling cost, MOQ, lead time, quality control.
1. How do modern eyewear factories control dimensional tolerances and warpage for TR-90 frames to ensure uniform lens fit across large production runs?
Why this matters: Buyers often receive frames with inconsistent lens gaps or stress that causes fitment issues with lenses. TR-90 (a nylon-based thermoplastic commonly called TR) is lightweight and resilient but susceptible to molding-induced residual stress and dimensional drift if process and tooling are not tightly controlled.
Factory controls and buyer checkpoints:
- Resin and pre-drying: Follow the resin technical data sheet. TR-90 pellets must be dried to the manufacturer-specified moisture level (typically to <0.1–0.2% moisture content) before molding to avoid voids and brittleness.
- Mold temperature control: Use consistent mold temperature across cavities via thermostatic control. Warpage is reduced by keeping mold temperature within the resin supplier's recommended range and avoiding large temperature gradients across the tool.
- Cavity balance and gate design: Balanced flow and properly designed gates reduce differential shrinkage. Multi-cavity tools must be flow-balanced and periodically validated with flow simulation (Moldflow or equivalent) and first-off inspection.
- Process stability and SPC: Implement Statistical Process Control for injection parameters (shot size, hold pressure, screw speed, cycle time). Track dimensional KPIs (e.g., temple length, frame front curvature, lens opening width) with control charts and set action limits at ±2 sigma for process adjustment and ±3 sigma for rejection thresholds.
- Tool maintenance and polishing: Mold wear changes dimensions over time. Schedule preventive maintenance, measure critical dimensions on the first 100, then each 1,000 parts; polish/microwork as needed to maintain the lens groove tolerances (typically within ±0.15 mm for snap-in lens systems; tighter if required for optical-grade sealed assemblies).
- Post-mold stress relief: Some factories use annealing ovens or controlled aging (temperature and humidity cycles) to relieve internal stress and stabilize part geometry before finishing operations.
Buyer actions: Request sample PPAP-style documentation (first article inspection), part specific dimensional drawings with critical tolerances, and periodic SPC reports. Specify allowable lens-fit tolerances in the tech pack (e.g., maximum lens gap, clip torque) so the factory can program tooling and process controls accordingly.
2. What injection molding parameters and mold maintenance practices reduce sink marks, flashing and short shots on TR sunglasses frames?
Why this matters: Surface defects and flashing lead to high scrap, extra hand trimming and inconsistent plating/painting results.
Key parameters and best practices used in modern eyewear factories:
- Material handling: Use closed conveying, hopper dryers and moisture sampling. TR resins are hygroscopic; moisture increases viscosity and creates burns or flow lines.
- Melt and mold temperature windows: Set barrel temperature zones and mold temperature according to resin datasheet. Rather than fixed numbers, modern factories refer to the resin manufacturer's processing window and validate with process capability studies.
- Injection/hold profile optimization: Proper injection speed, hold pressure and cooling time minimize sink marks. Use a dual-stage injection profile or segmented packing to fill thin ribs and lens grooves first, then pack bulk sections to avoid sinks.
- Ventilation and gate location: Insufficient venting causes burns and short shots. Proper gate placement and vent design prevent premature freezing or trapped air in long narrow features like temples and hinge pockets.
- Mold flow simulation and iterative tooling fixes: Simulate before tooling, then use scientific molding during try-out. For flashing, check parting line clearance and clamp tonnage; flash often indicates worn inserts or incorrect clamp pressure.
- Preventive mold maintenance: Regular inspection and replacement of wear inserts, vent channels cleaning, and polishing of cavities reduce defects. Keep a log for insert life and flash recurrence.
Buyer red flags: Low or no sample run data, factory unable to show cavity-specific scrap rates, or unwillingness to run fine-tuning trials. Ask for photos of first-off shots, and request a defect-rate target (e.g., <2% cosmetic defects for High Quality lines).
3. How do factories ensure coating adhesion and color consistency on TR-90 frames during mass finishing, plating or painting?
Why this matters: Buyers expect color consistency across seasons and batches, and good adhesion for plated or painted finishes on flexible TR frames.
Industrial controls and finishing steps:
- Surface prep: TR-90 requires surface activation because of low surface energy. Common methods include plasma treatment, corona treatment or chemical primers specifically formulated for nylon/thermoplastics before paint or vacuum metallization.
- Adhesion promoters and primers: Use validated primers compatible with downstream coatings. Adhesion is tested with cross-hatch adhesion testing (ASTM D3359) and pull tests for plated layers.
- Controlled painting and curing: Automated spray booths with programmable ovens ensure consistent film thickness and cure cycles. Track layer thickness with gauges; typical clearcoat thicknesses are controlled to avoid cracking on bending.
- Color management: Maintain an in-plant color lab with spectrophotometer-based matching (Delta E targets). Set a Delta E acceptance (commonly <1.5 for High Quality lines, <2.5 for fashion lines) and record batch pigment and lot numbers.
- Plating and vacuum processes: When metalized finishes are required, vacuum metallization or PVD coatings require tight control of pre-treatment and adhesion layers. Salt spray and abrasion tests (e.g., Taber abrasion) verify durability—ask for lab reports.
Buyer actions: Specify finish standards (Delta E, adhesion class, abrasion cycles). Request process flow sheets showing surface activation, primer, basecoat, topcoat and inspection points, and samples subjected to the same tests you expect for production (e.g., 72-hour salt fog for plated parts if outdoors exposure is expected).
4. What QC tests and pass/fail criteria should buyers require for TR sunglasses to meet ISO 12312-1 and industry optical safety requirements?
Why this matters: Optical safety and regulatory compliance are primary purchase drivers. Yet many answers online are generic—buyers need concrete test types and pass criteria to evaluate factory capability.
Core tests performed by modern eyewear factories and accredited labs:
- Filter category and visible light transmittance: ISO 12312-1 uses filter categories (0–4) based on visible light transmittance (VLT). Specify which category you require (sunglasses commonly use category 2 or 3 depending on intended use) and request lab certificates showing measured VLT.
- UV protection: Lenses and filters must meet UV requirements per ISO 12312-1 for UVA/UVB blocking. Request test reports from an accredited lab showing compliance across the relevant wavelength range.
- Impact resistance and mechanical tests: Verify compliance with applicable standards (ANSI Z80.3 for some markets) including drop-impact or high mass impact tests. Factories should provide test certificates or the ability to arrange third-party testing.
- Polarization verification: For polarized lenses, test the extinction ratio and ensure correct polarization axis. Ask for supplier polarization certificates and sample optical axis data.
- Durability tests: Abrasion resistance (ASTM or ISO equivalents), salt spray for plated frames, hinge cycle tests (e.g., 10,000 cycles) and color fastness to sweat and UV exposure. Define minimum acceptable cycles or abrasion loss per your product category.
- Dimensional and fit checks: Include lens seating torque tests, snap-in retention force and temple spring returns with pass/fail ranges defined in the tech pack.
Buyer checklist: Require copies of ISO 12312-1 and any applicable regional certifications from the factory or accredited labs. Define acceptance criteria in the purchase order (e.g., All lots must include a certificate of conformity to ISO 12312-1 and third-party UV test report). For new models, arrange pilot-run testing before mass production.
5. How do modern factories perform lens edging and snap-in tolerance control for polarized and coated lenses to prevent micro-scratches and frame strain?
Why this matters: Lens edging and insertion are chokepoints where optical coatings can be damaged and frames can be stressed, causing poor assembly yield and increased rework.
Standard factory practices:
- CNC lens edging and water-jet systems: Use digital lens edgers with programmed compensation for coating thickness and lens material. For polarized and multilayer-coated lenses, machines with soft or variable-pressure clamps and non-contact routing minimize micro-scratching.
- Edge chamfer and sealing: Proper edge geometry (micro-chamfer and rounded bead) reduces stress during snap-in. Specify edge radii and chamfer depth in the tech pack. For sealed designs, factories may use silicone gaskets or UV-curing adhesives applied in an ISO-classified clean area.
- Torque and retention metrics: Define lens retention force targets (e.g., snap-in torque range) and measure with torque gauges. For threaded or glued designs, specify adhesive type (structural UV adhesives) and cure profiles so coating compatibility is assured.
- Anti-scratch handling protocols: Dedicated operators, lint-free gloves, clean benches and protective films on coated lenses during handling reduce scratches. Automated handlers with suction cups and soft pads are used for higher-volume lines.
- Cable/hinge influence: For full-rim TR frames with tight tolerances, hinge insertion can deform thin areas. Use controlled torque drivers and fixtures to assemble hinges and perform post-assembly dimensional checks.
Buyer recommendations: Provide a lens specification sheet (thickness tolerance at specific radii, coating stack, polarization axis) and require sample assemblies. Define acceptable micro-scratch thresholds (magnification inspection level) and require inspection photos for first article approval.
6. What logistics, MOQ, lead-time and tooling cost breakdown should buyers expect when ordering custom TR sunglasses from an eyewear factory?
Why this matters: Hidden costs and unrealistic lead-time expectations cause project delays and budget overruns.
Typical cost and time elements (ranges depend on complexity and region):
- Tooling costs: Single-cavity injection mold inserts for frames can range from a few thousand to tens of thousands USD depending on complexity, cavity count and steel grade. Progressive molds with micro-features or multiple movable cores cost more. For plated or multi-material frames, additional inserts or overmolding tools may be required.
- Prototyping and sampling: Rapid prototyping (3D-printed prototypes) for fit-checks is inexpensive and fast (days), but final tooling samples require mold try-out and fine-tuning (usually 2–6 weeks for tool adjustments after commissioning).
- MOQ: Minimum order quantities vary by finishing and complexity. For custom finishes and plating, MOQ can be in the low hundreds per color; full tooling amortization and finishing setup often push MOQ to 300–1,000 pairs per SKU. Ask suppliers to list MOQ drivers (tooling amortization, plating bath set-up, color batch size).
- Lead times: After tooling sign-off, normal mass production lead times are typically 30–60 days for first production runs. Rush options exist but increase costs. Factor in additional lead time for third-party testing and certification if required.
- Per-unit cost breakdown: Roughly includes amortized tooling per-unit, raw material (TR pellets, metal parts, hinges), finishing (painting/plating), lenses (polarized or coated optics), QC, packaging and logistics. Request an itemized quote that separates tooling, sample charges, per-unit production, and testing fees.
- Logistics and compliance: Confirm the factory's export documentation capabilities, lead-time buffers for customs, and any certifications (REACH, RoHS where applicable for metal parts or plating) to avoid surprises.
Buyer negotiation tips: Ask for tiered pricing based on volume, require clear tooling amortization terms (e.g., tooling cost fully borne by buyer unless MOQ committed across multiple SKUs), and include penalty terms for late delivery or out-of-spec batches in the contract.
Concluding summary: Advantages of sourcing TR sunglasses from modern eyewear factories
Modern eyewear factories that apply controlled injection molding, CNC lens edging, surface activation (plasma or primer), automated finishing, and rigorous quality control (ISO 12312-1 testing, SPC charts, adhesion and abrasion testing) provide consistent product quality, scalable production, and compliant optical safety. The advantages for buyers include predictable tolerances and fit, repeatable color and finish, documented test certificates, and clearer upfront cost structures for tooling, MOQ and lead time. Factories with in-house labs and documented process flows reduce time to market and lower rework rates.
For a quote, first-sample plan or to discuss MOQ and tooling cost estimates, contact Karuson at www.karusonco.com or email nicole@karusonco.com. We can provide PPAP-style sample documentation, lab test coordination and a detailed cost breakdown for your TR sunglasses program.
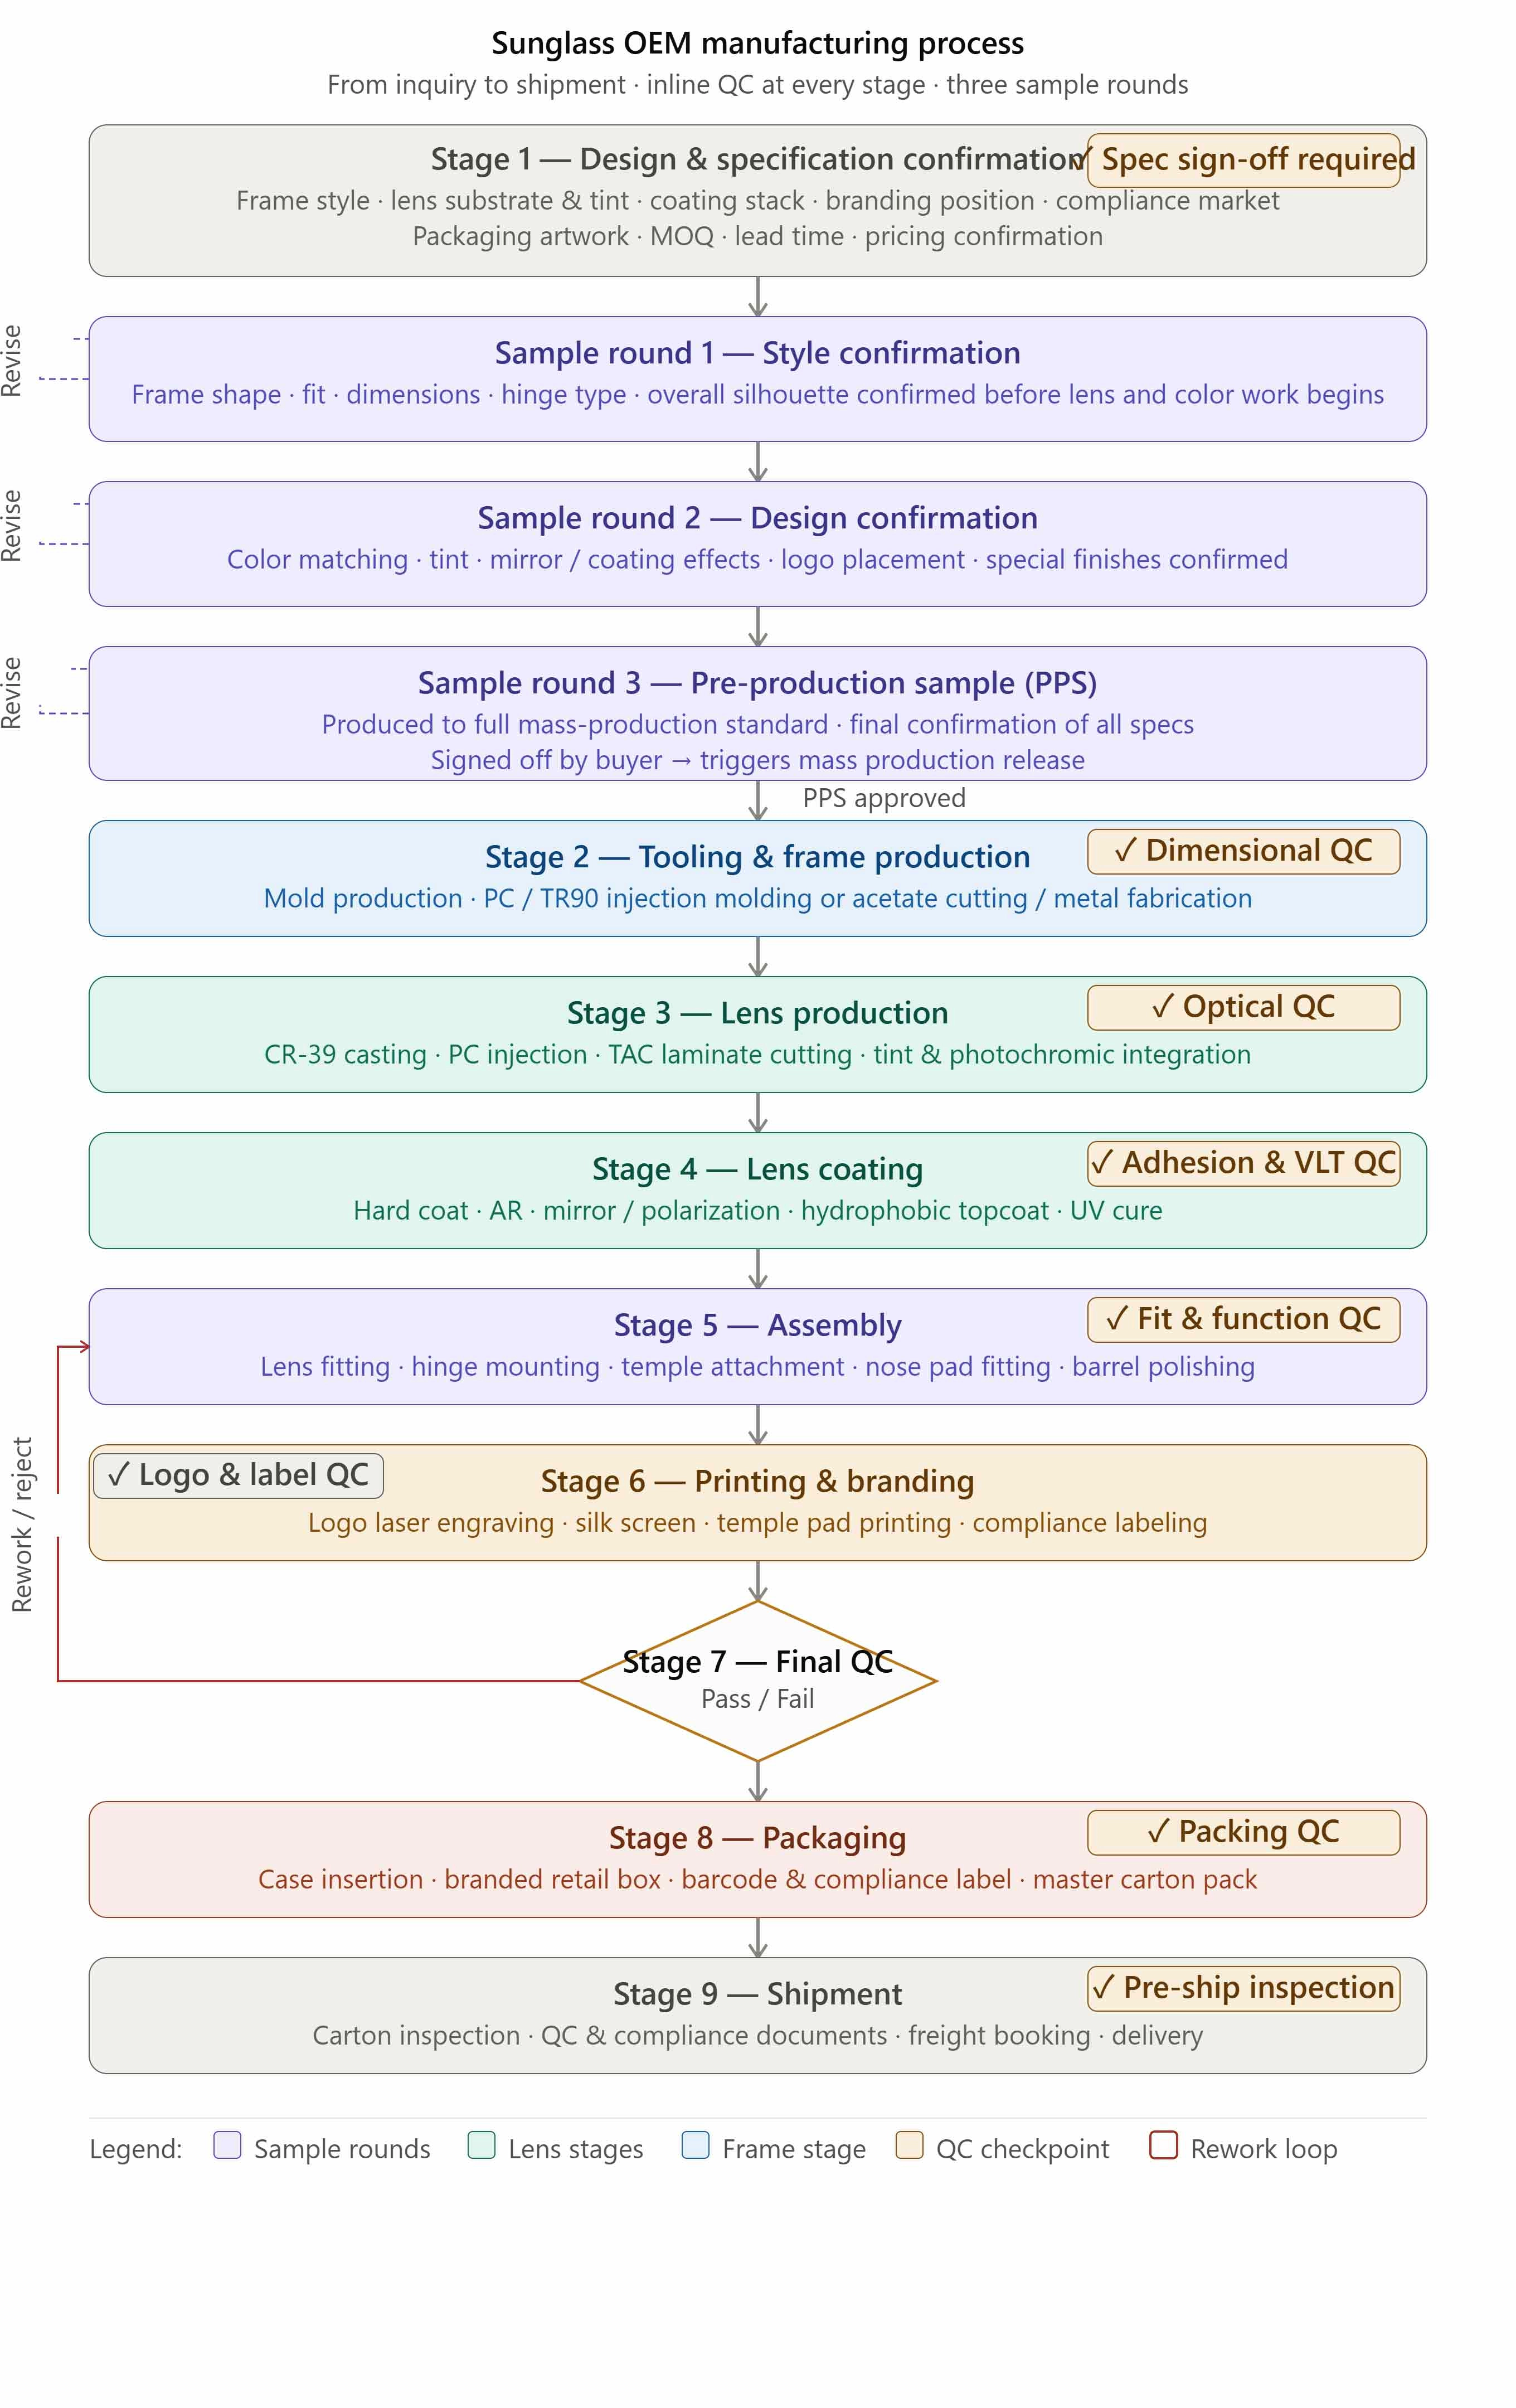
How Sunglasses Are Made: A Complete OEM Manufacturing Process Guide

Sunglass Lens Materials Compared: CR-39, PC, TAC, Nylon and Mineral Glass

Sunglass Lens Tint Categories Explained: A Complete Guide to Visible Light Transmittance for OEM Eyewear Brands

OEM Photochromic Lenses: Technology, Custom Options & B2B Sourcing Guide

Prescription Myopia Sunglass Lenses: Complete Guide on Optics, Production Process & Material Selection

Polarized Sunglasses with Anti-Seawater Coating: Technical OEM Specification Guide for Marine & Watersports Eyewear
You May Also Like
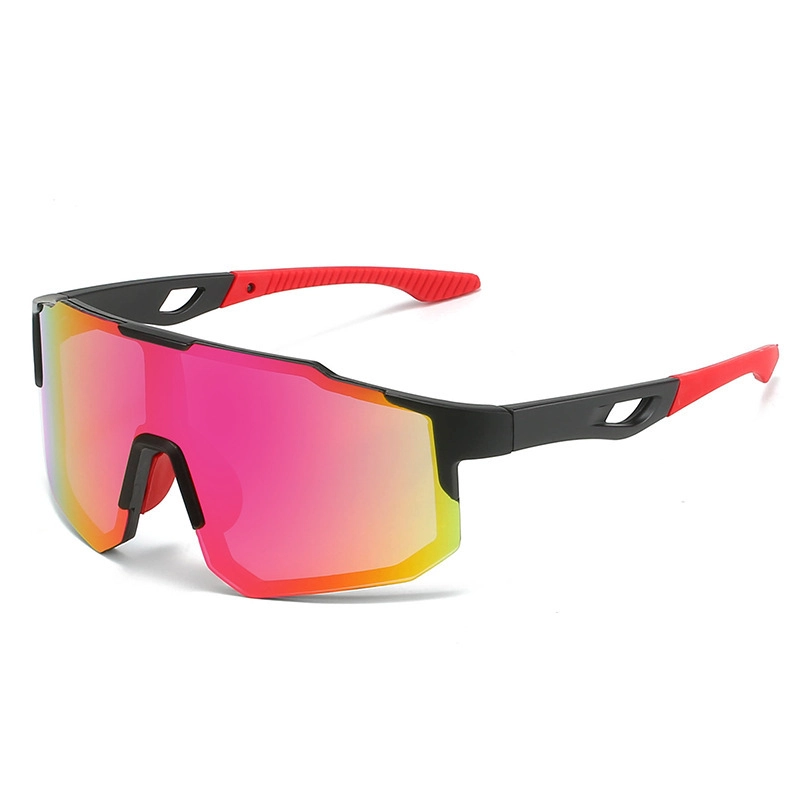
Wholesale Wraparound Sports Cycling Sunglasses, UV400 Impact‑Resistant Outdoor Goggles, Unisex Oversized One‑Piece Lens Shades
This wraparound sports cycling sunglasses features one‑piece oversized lens, ergonomic full‑wrap frame structure. Lightweight high‑toughness frame material, fitted soft textured nose pads and anti‑slip curved temple tips. Delivers UV400 sun protection and impact‑resistant performance. Multiple mirror‑coated lens & frame color options for men and women. Perfect inventory pick for sports shops, outdoor gear retailers, cross‑border sellers and brand partners. Support mixed‑color bulk order, logo engraving, neutral packing and full private‑label customization.
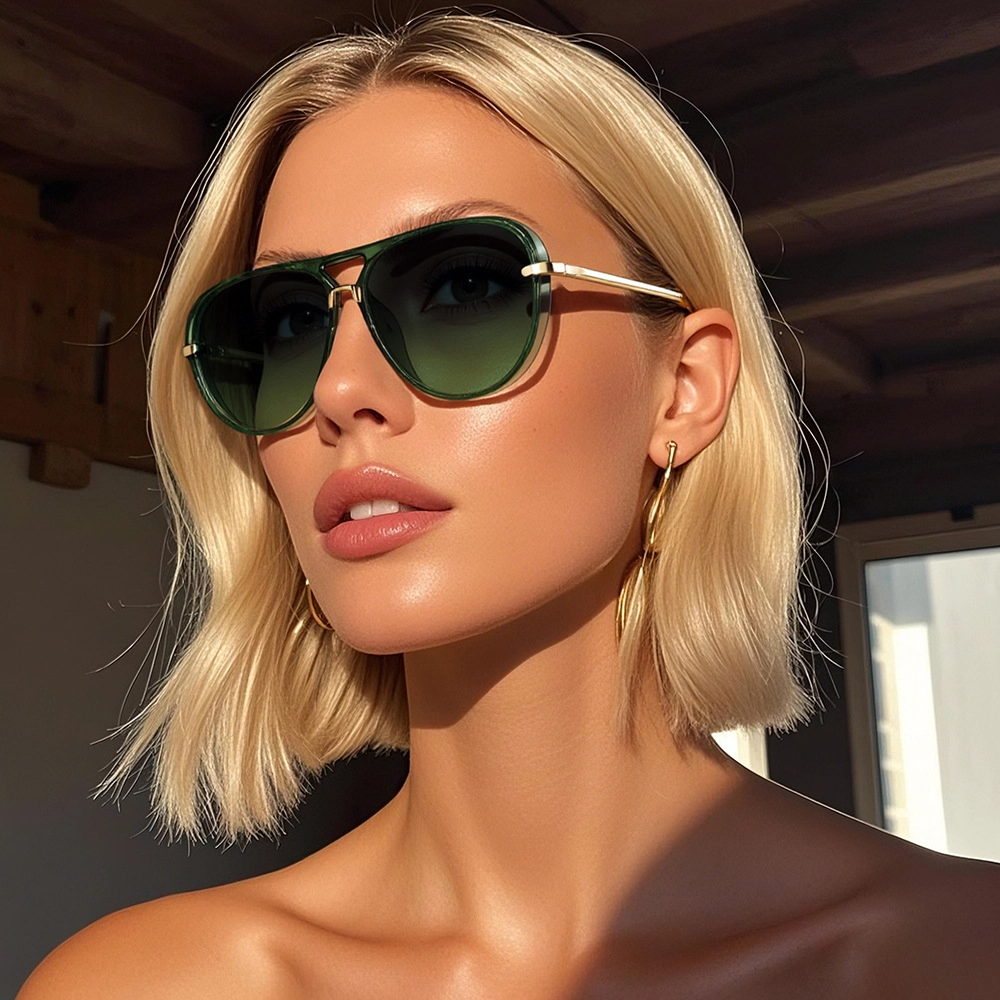
New Oversized Pilot Sunglasses for Women & Men – Retro Double-Bridge Aviator Sun Glasses, PC Frame, Fluorescent Green Gradient Lens, UV Protection
A bold, oversized take on the classic aviator. This double-bridge pilot frame pairs a wide PC front with slim gold-tone metal temples and a sculpted keyhole bridge for an elevated, editorial look. Offered in high-shine black, transparent amber, and the season's stand-out fluorescent green gradient. Lightweight at just 30.7 g, full UV protection, and a unisex fit that sells to both women's and men's channels. A strong add for boutiques, fashion accessories buyers, and online resellers chasing the current celebrity/influencer aviator trend.
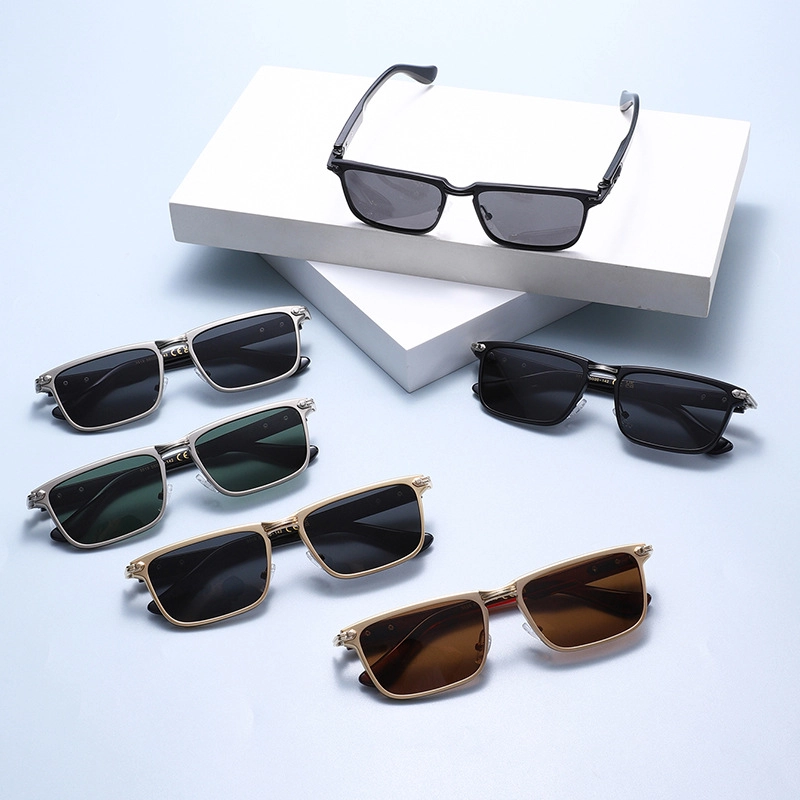
Wholesale Metal Square Polarized Sunglasses, Retro Sport Casual UV400 Sun Glasses Unisex Custom Logo Bulk for Physical Stores Distributors
Model KARMT008 is premium unisex metal square polarized sunglasses, blending retro styling with sport‑casual practicality. Sturdy full‑metal frame construction, multiple premium colorways in stock. Polarized UV400 lenses eliminate harsh glare for driving, outdoor sports and daily street wear.
Wholesale Retro Oval Sunglasses, European American Style UV400 Unisex Fashion Sun Shades Custom Logo
Model KARPC017 is vintage European‑American style oval sunglasses. Classic compact oval silhouette accented with premium metal decorative details on temples. Light‑weight frame weighs only 21g, equipped with UV400 protective tint lenses. Multiple trendy ready‑stock colorways for men and women.
Perfect inventory option for physical eyewear boutiques, apparel stores, cross‑border e‑commerce sellers and brand owners. Support mixed‑color assortment, temple laser engraving, neutral packing and full private‑label customization.
Get in touch with us
If you have any comments or good suggestions, please leave us a message; later our professional staff will contact you as soon as possible.
NEW DIMENSIONS IN EYEWEAR
Contact KARUSON
Email:
WhatsApp/Phone:
Address:
331 Section B, WanJia Creative Park , No. 1 BUXIA Road ,Tianhe District, Guangzhou City, Guangdong Province, China.

© 2026 KARUSON. All Rights Reserved.
Facebook
Instagram
YouTube
TikTok
Linkedin